Integrated treatment and resource recovery from palm oil mill effluent: technologies, performance, and future prospects
 0
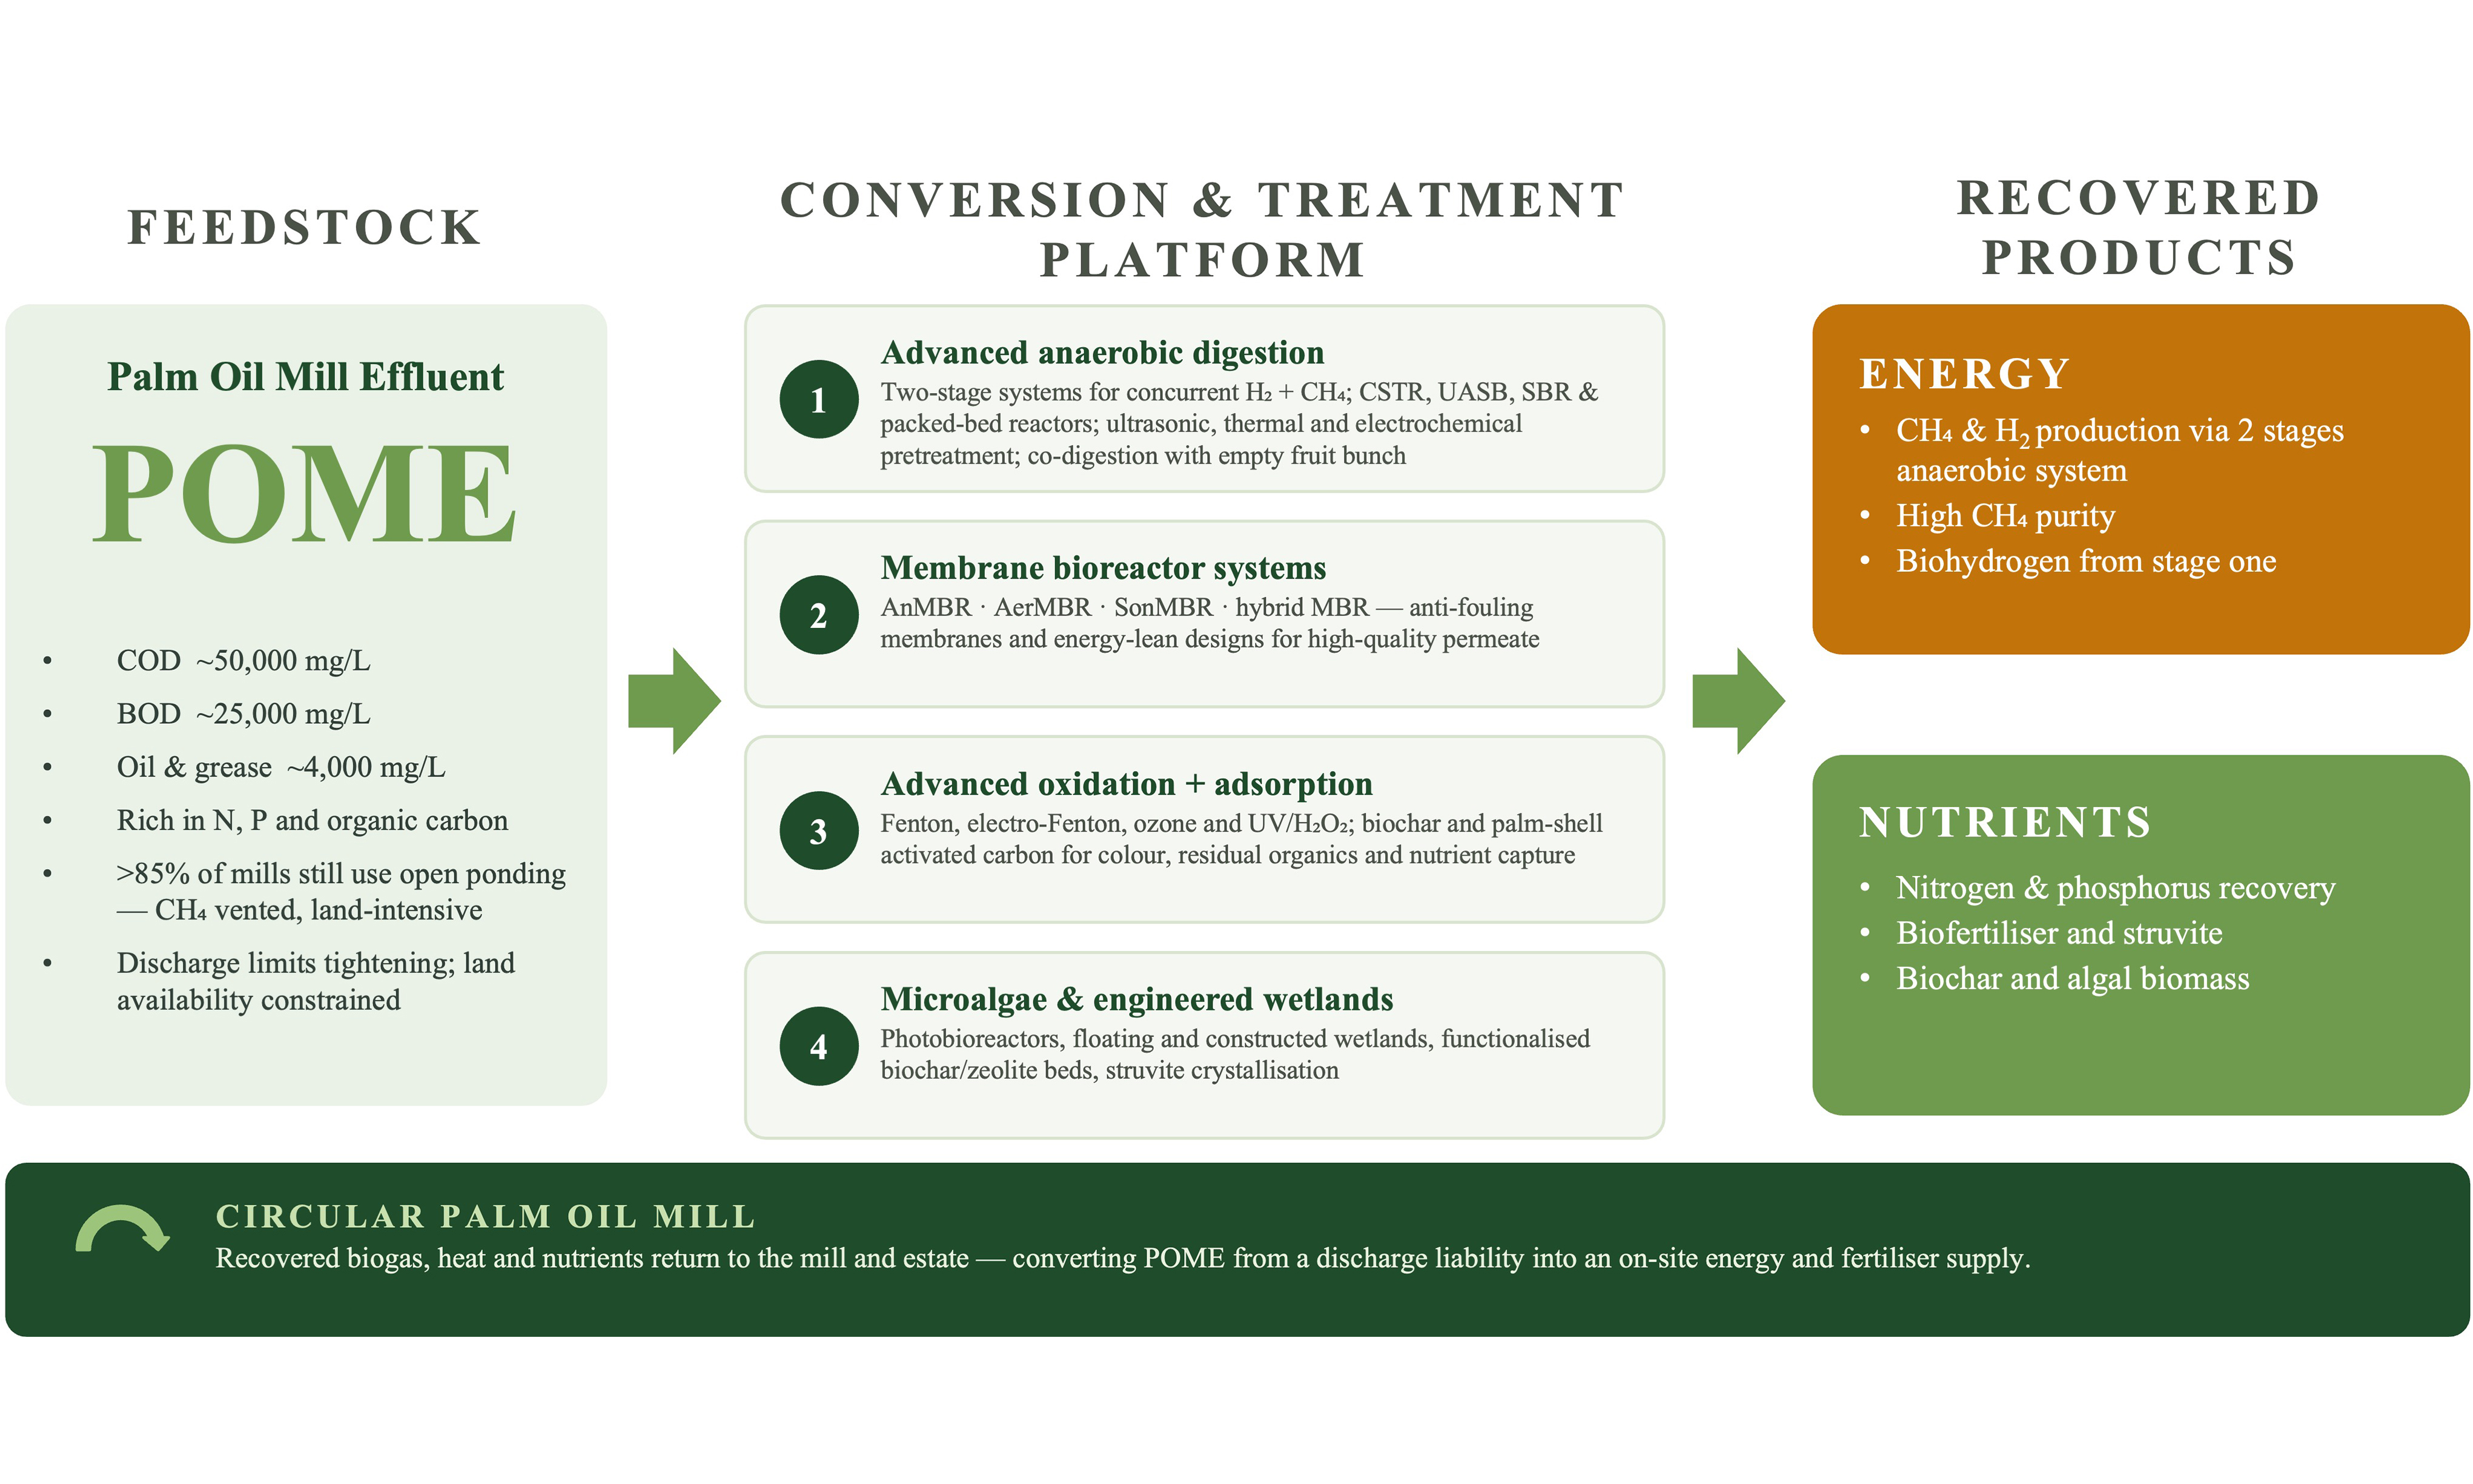
Graphical Abstract
Abstract
The palm oil industry contributes substantially to global vegetable oil production but generates large quantities of palm oil mill effluent (POME), which has traditionally been regarded as an environmental burden. POME production in Malaysia creates substantial opportunities for resource recovery. Current research extends beyond pollutant mitigation by integrating the recovery and valorization of energy-rich products, including methane and hydrogen, into established POME treatment systems. Microbial and biocatalytic conversion can generate recoverable products such as organic acids, whereas advanced oxidation processes can support integrated treatment by degrading or mineralizing persistent pollutants. Adsorption and microalgal cultivation also provide potential recovery pathways when captured nutrients and nutrient-loaded adsorbents are separated, harvested, and reused as biofertilizers. This review evaluates how resource-recovery concepts can be incorporated into current POME treatment technologies, with emphasis on methane and hydrogen production, nutrient recovery, and value-added product generation. Future research should demonstrate downstream product recovery and establish the economic viability and scalability of integrated POME treatment and resource-recovery systems.
Keywords


 Download PDF
INTRODUCTION
The palm oil industry supplies more than 35.0% of global vegetable oil production[1]. Malaysia is the world’s second-largest palm oil producer after Indonesia, with approximately 5.61 million hectares of oil palm plantations and production of 19.34 million tonnes of palm oil in 2024[2]. Palm oil processing generates solid and liquid by-products that can cause substantial environmental impacts when they are not managed appropriately[3]. Palm oil mill effluent (POME) has high biochemical oxygen demand and chemical oxygen demand, but its organic content also provides a feedstock for renewable energy and value-added chemical production. Advanced anaerobic digestion converts POME into biogas and can provide economic and environmental benefits[4]. Solid residues, including empty fruit bunches and palm kernel shells, can also be converted into biochar and activated carbon. Palm oil mill biomass comprises empty fruit bunches, palm mesocarp fibers, and palm kernel shells, whereas POME is the principal liquid residue. Processing one tonne of fresh fruit bunches generates approximately 22.0%-25.0% empty fruit bunches, 13.0%-16.0% mesocarp fibers, and 5.0%-7.0% palm kernel shells[3]. Empty fruit bunches have attracted attention as feedstocks for renewable energy and other applications. Mesocarp fibers and palm kernel shells have high calorific values and are commonly used in mill boilers, contributing to mill energy self-sufficiency. POME remains a major liquid-waste management challenge. Palm oil milling generates POME at approximately 0.7-0.9 m3 per tonne of fresh fruit bunches processed[5]. This review examines advances in technologies that convert palm oil processing residues into renewable energy or valuable products and examines the economic and technical constraints on scale-up.
POME is a brown, viscous wastewater generated mainly during fruit sterilization and crude palm oil clarification[4]. Its organic and inorganic constituents include carotene, lignin, phenolic compounds, tannins, carbohydrates, organic acids, and minerals, which require appropriate treatment. Methane released during uncontrolled anaerobic degradation contributes to greenhouse-gas emissions[6]. Untreated oily POME also contains high biochemical oxygen demand and chemical oxygen demand and can acidify and eutrophicate receiving waters[3]. POME treatment methods include biological, chemical, physical, and physicochemical processes[4], such as coagulation and flocculation[7], anaerobic and aerobic digestion[8], integrated sequential treatment[9], photocatalysis[10], and biofilm reactors[11]. Anaerobic digestion can simultaneously reduce the organic load and recover biogas. POME can also serve as a substrate for biological production of value-added chemicals because it contains phenolic compounds, organic acids, residual oils, and other biodegradable organics. Bacterial systems can degrade phenolic compounds[12], whereas microbial fermentation converts POME into succinic acids[13,14].
The current practices, limitations, and prospects for POME treatment and resource recovery are discussed. A Scopus search identified publications up to September 2026 on resource recovery from POME using the terms “POME” AND “removal” AND “recovery” in titles, abstracts, and keywords. The search retrieved 68 documents, comprising 56 research articles, 4 review papers, and 8 conference papers. The records were screened for POME treatment, pollutant removal and resource recovery. The review uses POME characteristics and regulatory requirements to evaluate ponding systems, anaerobic digestion, and bioreactors and to compare their treatment performance and limitations. It also examines scalability, waste-management costs, and nutrient-recovery potential. Adsorption, advanced oxidation processes, and integrated treatment systems are assessed as emerging approaches. This combined technological, environmental, regulatory, and economic analysis provides a structured assessment of POME management and recovery options.
GENERATION AND CHARACTERIZATION OF POME
Figure 1 summarizes the stages used to process fresh fruit bunches into crude palm oil. Fresh fruit bunches arrive at the loading bay and are sterilized with steam to loosen the fruits. Sterilizer condensate contains organic material leached from the fruits and is a major source of POME. Threshers then separate the fruits from the bunches, and digestion breaks down the fruit before oil extraction. The digested fruit is fed to a press, which produces crude palm oil. Clarification subsequently separates the oil from water and solids. Wastewater from the clarifier and decanter forms part of the POME stream. Aerobic and anaerobic ponds are commonly used to biodegrade organic matter and reduce the pollutant load before discharge[6].
Figure 1. Process flow diagram for a palm oil mill.
Steam generated in boilers fired with fibers and shells is used for fruit sterilization and oil extraction. Solid sludge from the milling stages is collected for disposal or further processing as a potential fertilizer or soil conditioner. POME accounts for approximately 60.0% of the waste generated during fresh-fruit-bunch processing[15]. Effective management is necessary because POME has high biochemical oxygen demand and chemical oxygen demand and can release methane when untreated. Biogas-recovery systems convert this liability into an energy resource[6]. Palm oil milling therefore combines mechanical, thermal, and biological operations, and integrated POME management is necessary for environmental compliance and sustainable production. POME was previously regarded primarily as an environmental problem but is increasingly recognized as a renewable-resource feedstock because of its high organic content. Anaerobic digestion can reduce its biochemical oxygen demand and chemical oxygen demand while producing methane and biohydrogen[16]. Improved anaerobic treatment systems can recover methane and support renewable-energy production. Treating POME as a resource rather than solely as a pollutant supports more sustainable palm oil production.
Raw POME is a dense, brown, viscous wastewater with an unpleasant odor and a high concentration of colloidal solids, making it a pollutant that can threaten water resources[17,18]. Water constitutes most of the stream, while soil particles, suspended solids, and residual oil account for less than 5.0%[19,20]. The physicochemical characteristics of raw POME demonstrate that it is a highly concentrated and heterogeneous wastewater requiring a combination of treatment mechanisms rather than a single-stage process, as shown in Table 1.
Properties of raw POME
| Parameters | Range | Discharge limit21] | |
| Turbidity (NTU) | 26,590 | - | [21] |
| Chemical oxygen demand (COD), mg/L | 50,000-78,290 | - | [8,22] |
| Ammoniacal-Nitrogen (NH3-N), mg/L | 87 ± 5.2 | 150 | [23] |
| pH | 4-5 | 5.0-9.0 | [22,24] |
| Suspended solids, mg/L | 18,000-47,375 | 400 | [22,24] |
| Total Solids, mg/L | 55,400 ± 200 | - | [25] |
| Total Nitrogen, mg/L | 1,200 ± 200 | 200 | [25] |
| Biochemical oxygen demand | 24,367-27,000 | 100 | [21,26] |
| Color, ADMI | 13,337.5 ± 1,178.6 | - | [27] |
| Temperature | - | 45 C | |
| Oil and grease | 4,000-14,110 | 50 | [8,26] |
Raw POME is a highly concentrated and heterogeneous wastewater by its high total dissolved solids, total solids, suspended solids, turbidity, and color intensity. Its COD concentration of 50,000-78,290 mg/L indicates an exceptionally high organic loading that could rapidly deplete dissolved oxygen if the effluent were discharged without adequate treatment[8,22]. The acidic pH of 4-5 is also below the Malaysian permissible discharge range of 5.0-9.0, reflecting the presence of residual free fatty acids and other acidic products generated during palm-oil processing[22,24]. Although the ammoniacal-nitrogen concentration of 87 mg/L is below the stipulated limit of 150 mg/L, the total nitrogen concentration of 1,200 ± 200 mg/L exceeds the corresponding limit of 200 mg/L by approximately 5-7 times[25]. This substantial difference indicates that nitrogen is predominantly present as organic nitrogen or other non-ammoniacal forms, which may subsequently be mineralized to ammonium during biological degradation. Moreover, the suspended-solids concentration exceeds the discharge limit of 400 mg/L by approximately 45-118 times, demonstrating that effective solids separation is essential before final discharge[22,24]. The absence of specific statutory limits for COD, total solids, total dissolved solids, turbidity, and color under the cited crude-palm-oil regulations should not be interpreted as evidence that these parameters are environmentally insignificant, because they directly influence oxygen depletion, light penetration, sludge accumulation, and the aesthetic quality of receiving waters. Considering the high solids and organic content, preliminary screening, oil recovery, sedimentation, decanting, or dissolved-air flotation should be employed first to remove coarse solids, residual oil, and settleable material. High-rate anaerobic digestion is subsequently appropriate for reducing the biodegradable organic load while recovering methane-rich biogas; however, anaerobic treatment alone is unlikely to achieve the required suspended-solids, nitrogen, color, and residual chemical oxygen demand (COD) levels. The anaerobic effluent should therefore undergo aerobic treatment to oxidize residual biodegradable compounds and facilitate ammonium nitrification. An anoxic denitrification stage, or alternatively partial nitritation-anammox for nitrogen-rich effluent with limited biodegradable carbon, may be required to achieve the total-nitrogen discharge limit. Coagulation-flocculation, electrocoagulation, or membrane separation can provide further removal of colloidal particles and residual suspended solids, whereas adsorption, advanced oxidation, or photocatalytic processes may be applied as tertiary polishing treatments for persistent color and refractory dissolved organics. Accordingly, an integrated treatment configuration comprising physical pretreatment, anaerobic digestion, aerobic-anoxic nitrogen removal, solids separation, and tertiary polishing is more technically appropriate than a single treatment process for managing the complex pollutant profile of raw POME.
POME is suitable for conversion into methane and hydrogen through advanced anaerobic digestion. Optimized operating conditions can increase gas yields and provide resource and economic benefits relative to conventional wastewater treatment, although the benefits depend on scale, energy prices, reactor configuration, and downstream biogas utilization. Organic fractions in POME can also serve as feedstock for biopolymers, organic acids, and biofuels, but the techno-economic performance of these recovery pathways remains insufficiently evaluated[4]. A transition from pollutant removal to resource recovery can reduce environmental impacts and improve economic performance when recovered energy and products offset treatment costs. Untreated POME depletes dissolved oxygen in receiving waters and alters aquatic microbial communities[18]. Anaerobic degradation releases odorous compounds that affect nearby communities[28]. Its high suspended-solids concentration, organic content, and acidic pH can also cause severe pollution[29]. POME exposure has reduced Daphnia magna reproduction[30] and caused sublethal effects in zebrafish embryos[31]. Direct discharge is therefore prohibited. Extreme rainfall can cause pond overflows and increase the risk of uncontrolled release.
Discharge limits define the physicochemical quality required for treated POME[32]. Chemical oxygen demand and biochemical oxygen demand remain the principal compliance challenges. Moderate influent chemical oxygen demand can support methane production in biogas-recovery systems[33], but final effluent must still meet regulatory limits. Residual color arises from suspended and dissolved compounds[34], and other anthropogenic inputs can complicate attribution of river pollution. Supplementary real-time monitoring would help mill operators verify compliance and identify abnormal discharges. Industry-wide implementation requires shared commitment from regulators and mill operators.
REVIEW OF ADVANCED POME TREATMENT AND RESOURCE RECOVERY TECHNOLOGIES
The transition from waste management to resource recovery offers a pathway towards more sustainable palm oil production. Treatment denotes removal or reduction of a constituent, whereas recovery requires harvesting, regeneration, or reuse of the captured resource. Anaerobic digestion recovers methane and hydrogen as usable energy products[35]. The summarized POME studies on advanced oxidation processes predominantly report degradation, mineralization, chemical oxygen demand reduction, or color removal and are therefore classified as pollutant-removal processes. Adsorption and biological nutrient uptake enable recovery only when the nutrient-bearing adsorbent or biomass is subsequently separated and reused or when nutrients are desorbed. More than 85.0% of palm oil mills use ponding systems for POME treatment[26]. A typical system comprises a de-oiling tank, acidification ponds, anaerobic ponds, and facultative or aerobic ponds. The aerated upper layer supports microorganisms that oxidize residual organic matter and reduce ammonia, odor, biochemical oxygen demand, and chemical oxygen demand. Mill capacity determines the number of ponds required[36]. Reported final chemical oxygen demand and biochemical oxygen demand concentrations are 100-1,725 mg/L and 100-610 mg/L, respectively[37]. Ponding systems are widely used as they require little energy, maintenance, process control, or mechanical mixing[15]. However, sludge accumulation reduces the effective pond volume and can increase the hydraulic retention time required for treatment[38]. Microbial degradation and natural aeration in successive ponds reduce pollutant concentrations before discharge. Ponding systems have low capital costs and simple operation, but they require large land areas and long hydraulic retention times. Other limitations include odor, mosquito breeding, variable effluent quality, and greenhouse-gas emissions when biogas from anaerobic ponds is not captured. These constraints can prevent consistent compliance with stringent discharge standards.
Advanced anaerobic digestion for methane and biohydrogen recovery
Closed anaerobic digesters have been developed to improve biogas production and address the limitations of open ponding systems. Anaerobic digestion involves hydrolysis, acidogenesis, acetogenesis, and methanogenesis through coordinated microbial activity[6]. Closed digesters provide greater process control and shorter hydraulic retention times than covered anaerobic ponds. Table 2 summarizes anaerobic reactors, pretreatment methods, feed conditions, operating parameters, and performance. The reported batch, sequencing-batch, and upflow anaerobic sludge blanket systems demonstrate that reactor design and operating conditions strongly affect chemical oxygen demand removal, biogas production, and methane yield.
Anaerobic treatments on POME for pollution mitigation and biogas production
| Treatment reactor | Pretreatment or enhancement | POME feed | Operating conditions | Performance | Ref. |
| Pretreatment of POME | |||||
| Anaerobic sequencing batch reactor | Acidified POME | Loading: 1.33 L/day OLR: 21.41 g-COD/L.day | Temperature: 54 ± 1 °C pH: 7.0-7.5 HRT: 3 days Motor speed: 80 rpm | COD removal: 71.0% TSS removal: 52.0% CH4 yield: 260.3 L/kg-COD CH4 content: 79.0% VFA consumption: > 80.0% | [39] |
| Anaerobic sequencing batch reactor | Ultrasonication pretreatment | OLR: 1.5-1.8 g/L·day Total solids: 6.0% (w/v) | Temperature: 30 °C pH: 7.0-7.5 HRT: 11 days Ultrasonication duration: 16.2 min Ultrasonication density: 0.88 W/mL | Maximum organic degradation: 96.0% Cumulative amount of biogas: 3,465 mL Methanogenic activity: 447 mL CH4/gVSS.day | [40] |
| Upflow anaerobic sludge blanket-hollow centered packed bed bioreactor | Thermal pretreatment and dewatering | OLR: 11.55-16.05 g-COD/L·day Solid loading: 40S:60L (v/v) | Temperature: 55 °C pH: 6.8-7.2 HRT: 2 days Thermal pretreatment duration: 1 h Thermal pretreatment temperature: 120 °C Dewatering duration: 16 h Dewatering temperature: 65 °C Dewatering motor speed: 2-5 rpm | COD removal: 97.5% BOD removal: 95.1% TSS removal: 94.5% Biogas production rate: 48 L/day CH4 content: 77.2% | [41] |
| Electrochemical oxidation batch reactor | Electrochemical oxidation pre-treatment | Inlet TS: 41573 ± 4846 mg/L | Temperature: 30 ± 0.5 °C SRT: 15 days EO current density: 17-27 mA/cm2 EO electrolysis time: 55-75 min EO NaCl concentration: 10 g/L | COD removal: 68.8% CH4 yield: 11.47 mL/g-COD added | [42] |
| Co-digestion of solid and liquid biomass | |||||
| Novel continuous reactor | Simultaneous outer liquid-state anaerobic digestion for POME and inner solid-state anaerobic digestion for empty fruit bunches | OLR for POME: 1.60-1.68 g-VS/L.day OLR for empty fruit bunches: 4.90-5.30 g-VS/L.day Flow rate for POME: 28 kg/day Flow rate for empty fruit bunches: 300-310 g/day NaOH/empty fruit bunches ratio: 7.0% (w/v) | Temperature: 55 and 70 °C HRT for POME: 25 days HRT for empty fruit bunches: 35 days | COD removal (55 °C): 87.0% COD removal (70 °C): 88.7% VS removal (55 °C): 79.6% VS removal (70 °C): 82.3% CH4 yield from POME and empty fruit bunches (55 °C): 476.61 and 125.84 mL/g-VS CH4 yield from POME and empty fruit bunches (70 °C): 507.07 and 123.12 mL/g-VS CH4 content from POME and empty fruit bunches (55 °C): 68.7% and 48.3% CH4 content from POME and empty fruit bunches (70 °C): 67.0% and 48.7% | [43] |
| Integrated upflow anaerobic sludge fixed-film | Biohydrogen production | COD-to-VSS feed ratio (F/M): 1.03/day Recycle flow rate: 54.49 L/day Feed flow rate: 2.51 L/day | Temperature: 57 °C pH: 5-5.5 HRT: 7 h Up-flow velocity: 1 m/h | COD removal: 35.9% H2 production: 10.39 L/day H2 yield: 0.95 L/g-CODremoved | [44] |
| Batch reactor | Co-digestion with empty fruit bunches | Initial organic concentration: 11 g-VS/L OLR: 0.31 g-VS/L.day Empty fruit bunches/POME ratio: 0.6/1 Empty fruit bunches/NaOH solution ratio: 1/19 | Temperature mesophilic: 35 °C Temperature thermophilic: 55 °C Duration: 35 days | COD removal: up to 77.0% Thermophilic CH4 production yield: 74 mL/g-VS Mesophilic CH4 production yield: approximately 60 mL/g-VS | [45] |
| Two-stage anaerobic system to produce hydrogen and methane | |||||
| Two-stage batch reactor | Stage 1: Hydrogenogenic Stage 2: Methanogenic Co-digestion with skim latex serum as a buffering agent | Initial organic concentration: 7 g-VS/L Skim latex serum/POME-VS mixing ratio: 55/45 (VS basis) | Temperature: 55 °C pH: 5.90-6.12 Duration: 30 days Buffer: 3 g/L NaHCO3 | H2 yield: 84.5 ± 0.7 mL/g-VSadded CH4 yield: 311.2 ± 8.0 mL/g-VSadded | [46] |
| Two-stage batch reactor | Stage 1: Thermophilic Stage 2: Mesophilic | Initial POME loading: 0.5 g-COD | Stage 1 temperature: 55 ± 3 °C Stage 2 temperature: 30 ± 3 °C Duration: 80 days | H2 yield: 106 mL/g-COD CH4 yield: 334 mL/g-COD | [8] |
| Integrated system: Continuous stirred tank reactor Anaerobic horizontal baffled channel reactor | Stage 1: Continuous stirred tank reactor Stage 2: Anaerobic horizontal baffled channel reactor | OLR stage 1: 25.40 g-COD/L⋅day OLR stage 2: 2.11 g-COD/L⋅day | Stage 1 temperature: 55 °C Stage 2 temperature: 33 °C Stage 1 HRT: 3 days Stage 2 HRT: 35 days | H2 yield: 86.0 mL/g-COD CH4 yield: 236.0 mL/g-COD H2 production rate: 2.2 L/Lreactor.day CH4 production rate: 0.53 L/Lreactor⋅day | [8] |
| Industrial-scale anaerobic lagoon digesters | |||||
| Covered lagoon digester with a hydraulic recirculation system | Industrial scale | OLR: 1.23 kg/m3.day Inlet TS: 46370 mg/L | Temperature: 45.4 °C | COD removal: 93.4% CH4 yield: 0.335 m3/kg-CODremoved | [47] |
| In-ground lagoon digester | Industrial scale | OLR: 1.30 ± 0.15 kg-COD/m3.day Recirculation ratio: 2.39 ± 0.74 | Temperature: 39 ± 1.3 °C pH: 7.45 ± 0.10 HRT: 64.04 ± 7.83 | COD removal: 78.7% ± 1.8% BOD removal: 88.47% ± 2.3% TS removal: 64.78% ± 6.0% Biogas production: 378,874.72 ± 67,967 Nm3/month CH4 yield: 0.250 ± 0.040 Nm3/kg-CODremoved CH4 content: 58.62% ± 1.3% | [48] |
Pre-treatment of POME
Acidified POME, the volatile-fatty-acid-rich digestate produced during the hydrogenogenic stage, has been treated in an anaerobic sequencing batch reactor[39]. At an optimal hydraulic retention time of 3 days, the process achieved a methane yield of 260.3 L/kg-COD, methane purity of 79.0%, chemical oxygen demand removal of 71.0%, total suspended solids removal of 52.0%, and volatile fatty acid consumption above 80.0%. However, chemical oxygen demand removal remained lower than that reported for a continuous stirred-tank reactor operated at a 5-day hydraulic retention time[49] and an upflow anaerobic sludge blanket reactor operated at a 2-day hydraulic retention time[50]. These comparisons demonstrate the importance of reactor configuration and operating conditions for acidified-POME treatment.
Ultrasonic pretreatment increased mean biogas production from 4.5 to 6.79 L/day and methane content from 73.0% to 85.0% relative to untreated POME[35,40]. Sonication disintegrated particles, increased organic-matter solubility and surface area, and improved mass transfer[51]. In a thermophilic upflow anaerobic sludge blanket-hollow-centered packed-bed bioreactor, thermal pretreatment and dewatering at a 40:60 solid-to-liquid loading produced 48 L/day of biogas with 77.2% methane and removed 97.5% of chemical oxygen demand, 95.1% of biochemical oxygen demand, and 94.5% of total suspended solids[41]. Stable operation was reflected by a consistently low volatile fatty acid-to-alkalinity ratio. Electrochemical oxidation before batch digestion of POME waste-activated sludge increased chemical oxygen demand removal from 37.1% to 68.8% and methane yield from 3.9 to 11.47 mL CH4/g-COD[42].
Co-digestion of solid and liquid biomass
A continuous reactor was developed to produce biogas from solid- and liquid-state anaerobic digestion in a single vessel[43]. The reactor contains an external chamber for liquid-state digestion of POME and an internal chamber for solid-state digestion of empty fruit bunches. Heat from POME digestion supports thermophilic digestion of the solid feedstock at 55 and 70 °C[43]. Maximum methane yields reached 507.07 mL CH4/g-VS from POME and 125.84 mL CH4/g-VS from NaOH-treated empty fruit bunches. NaOH pretreatment disrupted the lignocellulosic structure and increased methane production by approximately 14.1% relative to untreated biomass. The vertical configuration shown in Figure 2 further reduces energy use. Integrating solid and liquid digestion within one reactor reduces the required footprint and improves internal heat use, although commercial scalability and cost require further validation[43].
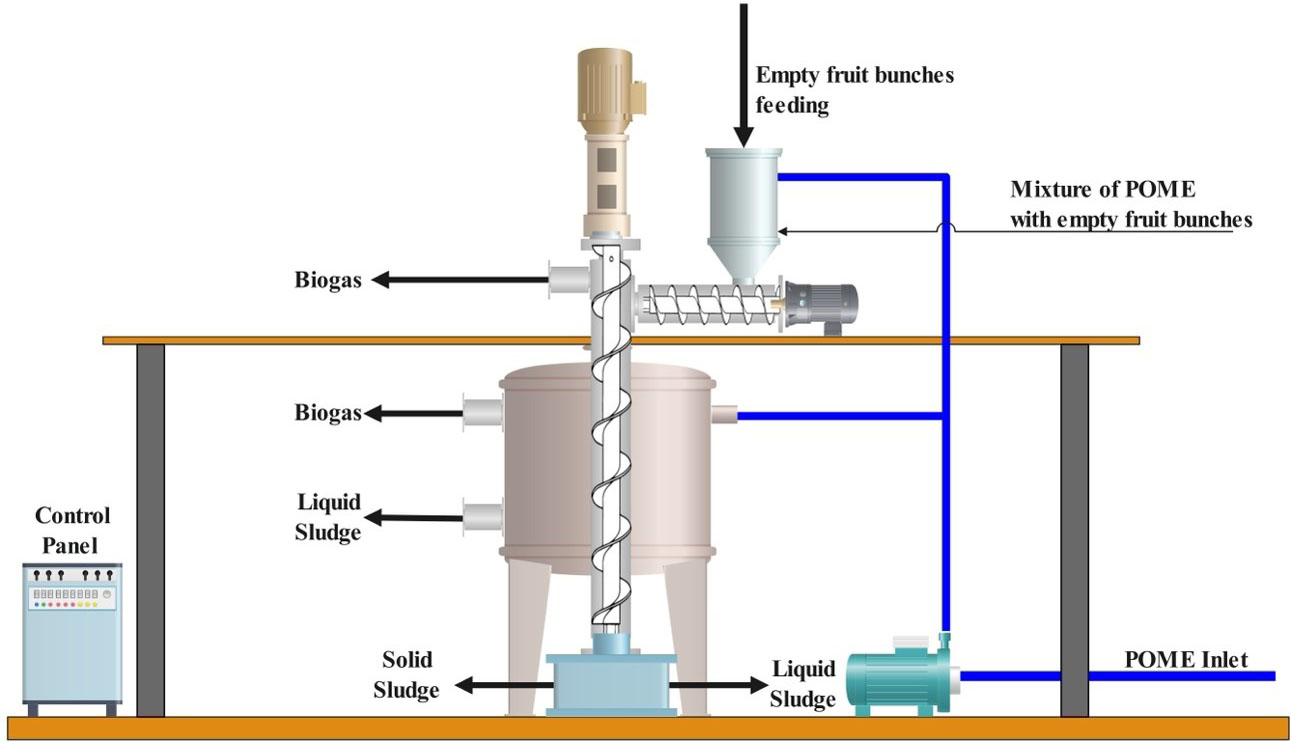
Figure 2. Vertical liquid and solid-state anaerobic digestion for biogas production. POME: Palm oil mill effluent.
An integrated upflow anaerobic sludge fixed-film reactor accommodated high organic loading rates and short hydraulic retention times during biohydrogen production from POME containing non-dissolved solids[44]. At 57 °C and a hydraulic retention time of 7 h, the reactor achieved a hydrogen yield of 0.95 L H2/g-COD removed and chemical oxygen demand removal of 35.9%. Co-digestion of POME with empty fruit bunches at a ratio of 1:0.6 removed up to 77.0% of chemical oxygen demand and produced 74 mL CH4/g-VS under Thermophilic conditions[45]. Combining carbon-rich empty fruit bunches with nutrient-rich POME improved substrate balance and anaerobic-digestion stability.
Two-stage anaerobic systems for hydrogen and methane production
A two-stage anaerobic system separates hydrogenogenic fermentation from methanogenesis to produce biohythane[46]. The system produced 84.5 mL H2/g-VS added in stage 1 and 311.2 mL CH4/g-VS added in stage 2[46]. Operating the stages at 55 °C and 30 °C, respectively, increased production to 106.13 mL H2/g-COD and 334.56 mL CH4/g-COD during batch fermentation of POME[8]. Under continuous operation, a thermophilic continuous stirred-tank reactor followed by a mesophilic anaerobic horizontal baffled-channel reactor produced 86.0 mL H2/g-COD and 236.0 mL CH4/g-COD and removed 66.3% of chemical oxygen demand at hydraulic retention times of 3 and 35 days, respectively[8].
Industrial-scale covered anaerobic lagoon digesters
Most studies have evaluated closed anaerobic digesters, whereas recent industrial-scale studies have examined covered lagoon digesters. A high-throughput lagoon with hydraulic recirculation achieved 93.4% chemical oxygen demand removal and a methane yield of 0.335 m3/kg-COD removed at an organic loading rate of 1.23 kg/m3·day, inlet total solids of 46,370 mg/L and 45.4 °C[47]. Four in-ground lagoon digesters operated under mesophilic conditions in Malaysia achieved methane yields of 0.250 ± 0.040 Nm3/kg-COD removed and chemical oxygen demand removal efficiencies of 78.7% ± 1.8%[48].
Membrane bioreactor system for enhanced energy recovery
Membrane bioreactor (MBR) technology combines biological degradation with membrane separation for POME treatment. The bioreactor degrades pollutants, while ultrafiltration or microfiltration membranes retain suspended solids, microorganisms, and other contaminants. This separation allows high biomass concentrations, a compact footprint, high-quality effluent, and effective removal of suspended solids, bacteria, and viruses[52]. MBRs use either external cross-flow or internal submerged membranes. In external systems, mixed liquor is pumped from the bioreactor through a separate membrane module. In submerged systems, the membrane is immersed directly in the bioreactor. Submerged configurations generally require less energy and space but are more susceptible to fouling at high biomass concentrations.
MBR configurations include aerobic MBRs, anaerobic MBRs, sonication-assisted MBRs, and hybrid MBRs[6]. Reactor configuration and operating conditions determine their suitability for specific treatment objectives. Submerged and cross-flow systems combined with ultrasonic pretreatment can mitigate fouling and improve biogas yield and operational stability[53,54]. Hybrid systems containing activated carbon can improve contaminant removal and fouling resistance. Their contribution to nutrient recovery depends on subsequent separation and reuse of the captured nutrients. High capital cost, membrane replacement, fouling control, and energy demand remain important barriers to commercial application. Table 3 summarizes applications of MBRs for POME treatment.
POME treatment for pollution mitigation and biogas production using membrane bioreactors
| Membrane bioreactors | Pretreatment or enhancement | POME feed | Operating conditions | Performance | Ref. |
| Anaerobic external cross-flow ultrafiltration membrane bioreactor | Integrated ultrasonic membrane anaerobic system | COD feed: 165,200 g/m3 SS: 24,925 g/m3 VSS: 17,440 g/m3 | Temperature: 70 °C Pressure: 2.5 bar pH: 4.25-4.95 HRT: 7 days Membrane: 4 tubular modules with a total effective area of 0.185 m2 Sonication time: 3 h | COD removal: 94.4% CH4 production: 24.9 m3 | [53] |
| Anaerobic external cross-flow ultrafiltration membrane bioreactor | Integrated ultrasonic membrane anaerobic system | OLR: 1-11 kg-COD/m3.day COD feed: 65,000-88,100 mg/L | Pressure: 1.5-2 bar pH: 6.7-7.8 HRT: 7.5-100.4 days SRT: 12.1- 500 days Membrane: 2 tubular modules with a total effective area of 0.024 m2 Multi-frequency ultrasonic transducers: 20 kHz | COD removal: 96.6%-98.4% Biogas yield: 0.26-0.87 L/g-COD.day CH4 yield: 0.19-0.60 L/g-COD.day CH4 content: 68.8%-73.0% | [54] |
| Aerobic submerged chlorinated polyethylene membrane bioreactor | Pilot scale | Pretreatment: anaerobic digestion and facultative treatment in the ponding system MLSS: 6,000-8,000 mg/L MLVSS: 4,000-5,500 mg/L | Temperature: 27-30 °C HRT: 15 h SRT: 60 days Air flow: 2 m3/min Dissolved oxygen: 4-6 mg/L Membrane: 40 flat-sheet membranes | COD removal: 30.0% TS removal: 4.0% | [55] |
| Anaerobic submerged polysulfone membrane bioreactor | High-rate operation with a prolonged SRT and operating period Two-stage membrane bioreactor Anaerobic hydrolytic reactor before the membrane bioreactor | OLR: 42.6-99.1 kg-COD/m3.day COD feed: 190 g/L TS: 33.6 g/L SS: 23.3 g/L VS: 12.8 g/L | Temperature: 35 ± 5 °C Duration: 270 days HRT: 1.5-3.3 days Membrane: 1 hollow fiber module with a total effective area of 0.025 m2 at each stage Gas sparging: 1.25 L/h Internal recirculation: 1.8-5.5 days | COD removal: 70.0% Biogas production: 21.2-28.5 L/day CH4 production: 15.4-19.8 L/day CH4 content: 66.0%-76.0% | [56] |
| Anaerobic external polytetrafluoroethylene microfiltration membrane bioreactor | Thermophilic conditions | OLR: 2.0-10 kg-COD/m3.day COD feed: 60 g/L MLSS: 17.5-29.4 g/L MLVSS: 11.1-20.9 g/L | Temperature: 55 °C Duration: 203 days Membrane: 1 hollow fiber module with a total effective area of 0.1 m2 | COD removal: 93.0%-98.0% CH4 yield: 0.19-0.56 m3/kg-CODremoved CH4 content: 65.1% ± 2.2% | [57] |
| Hybrid anaerobic submerged polyethersulfone membrane bioreactor | Addition of powdered activated carbon | COD feed: 16,449 ± 7,840 mg/L MLSS: 9,500-12,500 mg/L MLVSS: 8,350-9,700 mg/L | Temperature: 45 °C pH: 7.8 ± 0.1 HRT: 12.5 days SRT: 30 days Powder activated carbon: 5 g/L with 75.72 ± 1.52 μm particle size | COD removal: 89.5% ± 2.5% Biogas yield: 137 ± 7 mL/h | [58] |
Aerobic (AerMBR) and anaerobic (AnMBR) membrane bioreactors
A pilot-scale aerobic MBR fitted with a submerged chlorinated-polyethylene flat-sheet membrane treated POME after anaerobic digestion and facultative pond treatment. The system removed up to 30.0% of chemical oxygen demand and 4.0% of total solids while enabling analysis of microbial-community composition[55]. A simulated power outage altered the microbial profile during shutdown, but the community recovered after operation resumed. An anaerobic MBR containing a submerged hollow-fiber polysulfone membrane with an effective area of 0.025 m2 was evaluated in single-stage and two-stage configurations at high loading rates, long solids retention times, and extended operating periods[56,59]. An anaerobic hydrolytic reactor provided pretreatment before the MBR. Coupling biological treatment with membrane filtration achieved 70.0% chemical oxygen demand removal, of which membrane separation contributed an additional 23.9%-34.7%[56].
Sonication and hybrid membrane bioreactors
Sonication-assisted MBRs use ultrasonic cavitation to break complex organic matter into smaller compounds. Operating two tubular modules with a combined area of 0.024 m2 achieved 96.6%-98.4% chemical oxygen demand removal, a methane yield of 0.19-0.60 L/g-COD·day, and methane content of 68.8%-73.0%[54]. At a 7-day hydraulic retention time, an ultrasonic-assisted membrane anaerobic system achieved 94.4% COD removal and reported methane production of 24.9 m3 from high-strength decanter POME, compared with 82.8% COD removal and 9 m3 of methane from final-discharge-pond POME; the reactor was operated for 5 h/day, including 3 h of sonication[53]. Hybrid MBRs improve anaerobic digestion by adding powdered activated carbon to a submerged polyethersulfone membrane bioreactor[58]. Activated carbon with a particle size of approximately 75 μm increased chemical oxygen demand removal to 89.5% and produced biogas at 137 mL/h[58]. The adsorbent increased floc size, reduced natural organic matter, and mitigated membrane fouling. Incorporating biosorbents can similarly improve fouling resistance and contaminant removal[60]. An external polytetrafluoroethylene hollow-fiber membrane operated under thermophilic conditions for more than 200 days achieved 93.0%-98.0% chemical oxygen demand removal, methane yields of 0.19-0.56 m3/kg-COD removed, and methane content of 65.0%[57].
POME treatment by adsorption
Adsorption has been widely studied for POME treatment using activated carbon, biochar, and modified natural adsorbents. The POME-specific studies in Table 4 primarily report removal of color, chemical oxygen demand, biochemical oxygen demand, total suspended solids, oil and grease, ammoniacal nitrogen, metals, or nutrients[34]. Adsorption enables recovery only when nutrients are subsequently desorbed and concentrated, the adsorbent is regenerated through a controlled recovery step, or a nutrient-loaded adsorbent is demonstrated to be safe and effective for agricultural reuse. These downstream outcomes remain insufficiently quantified in POME-specific studies. POME contains a high organic load, colloidal material, and oil and grease that can restrict treatment performance[18,69]. Adsorption transfers an adsorbate from the liquid phase to the surface or pores of an adsorbent[70]. Reversible interactions allow adsorbent regeneration through desorption[71,72]. Direct use of nutrient-loaded adsorbents as soil amendments or fertilizers requires evidence of nutrient availability, agronomic benefit, and environmental safety.
POME-specific studies on adsorbent-based treatment and pollutant removal
| Adsorbent | Operating conditions | Performance | Ref. |
| Boiler fly ash activated with (2.0% v/v) HNO3 | Mesh size: 425μm and 850μm Dosage: 10, 30, 40 and 60g Volume: 300ml Duration: 60 min pH: 6.4 | Sorption trend : BOD > Color > TSS | [61] |
| Palm kernel shell | pH: 3-11 Adsorbent dosage: 2-10 g/L Contact time: 2-6 h | Color removal: >99.7% COD removal: 80.3-85.0% | [62] |
| Oil palm trunk | Adsorbent dosage: 3 g pH: 8 Agitation speed: 150 rpm Contact time: 24 h | COD removal: 49.5% | [63] |
| Activated carbon derived from palm kernel shell | Adsorbent dosage: 0-120 g/L Agitation speed: 150 rpm Contact time: 0-36 h pH: 9 | Color removal: 97.0% TSS removal: 90.0% COD removal: 68.0% BOD removal: 83.0% | [64] |
| Banana and orange peel biochar | Dosage: 10 g/L Time: 3 days | BOD removal: 46.0% COD removal: 52.0% TSS removal: 18.0% O&G removal: 57.0% | [65] |
| Esterified sago bark fiber waste | Adsorbent dosage: 0.5-4.0 g sago bark and esterified sago bark in 100 mL POME pH: 2, 4.18, 7, 8, 10 Temperature: 30 °C Agitation speed: 200 rpm Contact time: 24 h | O&G removal: 57.7% (sago bark), 80.2% (esterified sago bark) | [66] |
| Empty fruit bunch | Adsorbent dosage: 50 g/L pH:8.56 Agitation speed: 200 rpm Contact time: 60 min Activation: Temperature: 900 °C Duration: 15 min Steam flow rate: 2-10 mL/min | Manganese (Mn) removal: 95.0% Hydrogen sulphide (H2S) removal: 90.0% | [67] |
| Thermally oxidized de-oiled spent bleaching earth | Dosage: 50 g/L Duration: 120 min | Nutrient adsorption: NH3: 3.7% P: 80.0% Zn: 7.3% Mn: 30.0% Fe: 13.6% | [68] |
POME-specific studies have evaluated adsorbents including chitosan-based materials, lignocellulosic biomass, activated carbon, zeolite, palm biomass-derived materials, and other composites for pollutant removal and final-effluent polishing. Montmorillonite has been applied for POME polishing with high COD and color removal[73], while palm oil boiler fly ash, palm-kernel-shell activated carbon, oil-palm-trunk material, fruit-peel biochar, coconut-shell activated carbon, and esterified sago-bark fiber have been investigated for removal of color, COD, BOD, TSS, oil and grease, and related contaminants[61-63]. Magnetic or composite adsorbents have also been investigated for POME polishing because they can facilitate separation of the sorbent after treatment. Chitosan-magnetic composites have been reported to remove turbidity, total suspended solids and COD by 98.8%, 97.6% and 62.5%, respectively, at pH 6 and dosage 250 mg/L from POME[74], while composite materials derived from activated cow bone powder, coconut shell, and zeolite have been evaluated for reducing COD and NH3-N[75]. Their future value for resource recovery will depend on demonstrating controlled desorption or regeneration, nutrient concentration in a reusable stream, repeated-cycle performance, or safe agronomic reuse of the nutrient-loaded material.
Anaerobically treated POME contains 480 mg/L total Kjeldahl nitrogen, 361 mg/L phosphorus, 28,356 mg/L potassium, and 348 mg/L iron. Malaysian refineries also generate 221,000 tonnes of spent bleaching earth annually, much of which is landfilled or used in cement production[68]. Thermally oxidized de-oiled spent bleaching earth, produced by heating de-oiled clay at 1,000 °C, was evaluated as a low-cost sorbent for nutrient recovery from anaerobically digested POME. At 50 g/L and 120 min, it recovered 80.0% of phosphorus, 30.0% of manganese, 13.6% of iron, 7.3% of zinc, and 3.7% of ammonia. The nutrient-loaded clay was proposed as a plantation soil conditioner, linking refinery and mill residues with agricultural reuse[68]. Table 4 summarizes POME-specific adsorption studies.
Nutrient removal from POME using plants and microalgae
Cultivation of microalgae and aquatic plants combines wastewater treatment with biological nutrient uptake [Table 5]. Reported POME media contain chemical oxygen demand concentrations of 198-2,900 mg/L, phosphate concentrations of 49-53 mg/L, ammonium concentrations of 29-99 mg/L, total nitrogen concentrations of up to 330 mg/L, and total organic carbon concentrations of up to 1,400 mg/L. Raw POME is commonly diluted to 5.0%-75.0% (v/v) to balance nutrient availability against inhibition by excessive organic loading[76]. Chlamydomonas sp. was cultivated for 16 days under a 12 h light/12 h dark cycle, with 100.0% ammonium removal, 82%-100.0% nitrate removal, and 16.7%-33.2% COD removal[76]. Scenedesmus sp. was cultivated for 30 days and achieved a maximum COD removal of 57.0%. Complete ammonium removal was achieved within 5-10 days under the conditions listed in Table 5[77]. Phosphate removal reached 91.0% under a 16 h light/8 h dark cycle at an organic loading rate of 11.67 mg COD L-1 day-1[77].
Nutrient removal and uptake from POME by plants and microalgae and the associated recovery potential
| Plants and microalgae | Operating conditions | Performance/results | Ref. |
| Scenedesmus sp. and Chlorella sp. | POME characterization: COD: 2,900 mg/L TN: 330 mg/L TOC: 1,400 mg/L Stage 1: POME treatment with Scenedesmus sp. A 30.0% (v/v) inoculum was added to the diluted POME at a dilution rate of 84.0% (v/v) Stage 2: CO2 fixation by Chlorella sp. with a 30.0% (v/v) inoculum Duration: 25 days | TN: 86.0% Reactive Phosphate: 85.0% TOC: 77.0% COD: 48.0% | [29] |
| Chlamydomonas sp. | POME characterization: pH 7 COD: 349-2,012 mg/L Phosphate (PO43-): 49-53 mg/L, Ammonium (NH4+): 29-99 mg/L, Magnesium (Mg2+): 292 mg/L POME dilution ratios: 75.0%, 50.0%, 25.0%, and 0.0% (v/v) Microalgal inoculum: 20.0% (v/v) / 200 mgL-1 dry biomass Photoperiod: 12 h light/12 h dark cycle at room temperature for 16 days Sampling interval: every two days | Ammonium removal (NH4+): 100.0% Nitrate (NO3-): 82%-100.0% Phosphate (PO43-): 66.0%-89.0% COD: 16.7%-33.2% | [76] |
| Scenedesmus sp. | Cultivation period: 30 days Microalgal inoculum: 20.0% (v/v) / 200 mgL-1 dry biomass Photoperiods: 12 h light/12 h dark, 16 h light/8 h dark 24 h light/0 h dark, continuous light Sampling interval: every five days | COD removal: Maximum COD removal: 57.0% Duration: 30 days Loading rate: 61.67 mg L-1d-1 NH4+ removal: Loading rate: 11.67 mg COD L-1 day-1 Removal: 100% Duration: 5 days under 12 h light:12 h dark. Duration: 10 days under 24 h light:0 h dark and 16 h light:8 h dark Loading rate: 36.67 mg COD L-1 day-1 Removal: 100% Duration: approximately 10 days Loading rate: 61.67 mg COD L-1 day-1 Removal: 100% Duration: 10 days under 16:8 and 12:12 photoperiods. PO43- removal: Loading rate: 11.67 mg COD L-1 day-1 Removal: 91%, Photoperiods: 16 h light:8 h dark | [77] |
| Chlamydomonas incerta | POME concentration: COD: 250 mg/L Duration: 28 days Chlamydomonas incerta inoculation: 2.0% (v/v) | COD removal: 67.4% | [78] |
| Azolla pinnata | COD: 35, 70, 110, and 200 mg/L A. pinnata: 5 g | COD uptake: 4.6, 7.3, 9.5 and 12.5 mg/g | [79] |
| Lemna minor Azolla pinnata | A. pinnata: 5 g L. minor: 2 g POME volume: 2 L COD: 198 mg/L, Nitrates: 4.3 mg/L pH: 9.53 Phosphate: 4 mg/L Ammonia: 2.98 mg/L dilutions (2.5%, 5.0%, 10.0%, 15.0%) Duration: 10 days | 5.0% POME dilution Ammonia removal by A. pinnata (98.0%) L. minor (95.5%) 10.0% POME dilution Phosphate removal by A. pinnata (93.3%) L. minor (86.7%) 15.0% POME dilution: COD removal by L. minor (78.0%) A. pinnata (66.0%) | [80] |
The POME-specific studies quantify removal or uptake of ammonium, nitrate, phosphate, total nitrogen, chemical oxygen demand, and biochemical oxygen demand. Chlorella sp.[29,81], Chlamydomonas sp.[76], Scenedesmus sp.[77], Azolla pinnata[79], and Lemna minor[80] have been evaluated because they grow in nutrient-rich media and assimilate nitrogen and phosphorus. Chlorella vulgaris and Scenedesmus sp. achieved high removal of nitrogen- and phosphorus-containing compounds[77,81]. Biological uptake creates a potential recovery pathway by transferring nutrients into harvestable biomass. Harvested Azolla biomass has potential use as a biofertilizer[79]. Raw POME is commonly diluted to provide suitable growth conditions[76]. Chlamydomonas sp. achieved 100.0% ammonium and nitrate removal, whereas Scenedesmus sp. achieved 100.0% ammonium and 91.0% phosphate removal[76,77]. Treatment with a 30.0% Scenedesmus inoculum in 84.0% diluted POME, followed by Chlorella at the same inoculum ratio, removed up to 86.0% of total nitrogen, 85.0% of reactive phosphate, and nearly 50.0% of chemical oxygen demand over 25 days[29]. These results demonstrate nutrient assimilation, but recovery requires harvesting and productive use of the resulting biomass. The aquatic macrophytes Azolla pinnata and Lemna minor demonstrated dilution-dependent removal of nutrients and organic matter from POME[80]. In a 10-day greenhouse experiment, 5 g of A. pinnata and 2 g of L. minor were cultivated separately in 2 L of POME diluted to 5.0%-15.0%. The highest ammonia removal occurred at 5.0% POME, reaching 98.0% with A. pinnata and 95.5% with L. minor. At 10.0% POME, A. pinnata also achieved greater phosphate removal than L. minor, with efficiencies of 93.3% and 86.7%, respectively[80]. Organic-matter removal followed a different pattern. At 15.0% POME, L. minor achieved 78.0% COD removal, compared with 66.0% for A. pinnata. These results demonstrate that the optimum POME concentration depends on both the target contaminant and the selected plant species: A. pinnata performed better for ammonia and phosphate removal, whereas L. minor provided greater COD removal at the highest dilution tested. Both species therefore offer complementary functions in POME polishing.
Advanced oxidation processes for POME pollutant removal and polishing
AOPs have attracted increasing attention for POME treatment due to their ability to generate highly reactive species capable of degrading refractory organic compounds that remain after conventional biological treatment. The reported performance summarized in Table 6 varies considerably according to the characteristics of the POME matrix, oxidant or catalyst dosage, reaction time, pH, irradiation intensity and the extent of pretreatment applied before the AOP stage. This variability indicates that direct comparison of removal efficiencies should consider both the initial wastewater strength and whether raw, diluted, anaerobically treated or final-discharge POME was used.
Advanced oxidation processes for POME treatment
| AOP configuration | Operating conditions | Performance | Ref |
| Photocatalytic fuel cell, ZnO/Zn-Pt | pH: 7; duration: 6 h Light: 1,300 lx ZnO/Zn photoanode and Pt cathode | COD removal: ~ 74.0% | [82] |
| Thermally activated persulfate | Temperature: 67.4 °C S2O82-/COD ratio: 9.8 Duration: 120 min | COD: 85.7% Color removal: 85.7% Reported cost: RM 0.94 L-1 | [83] |
| Ozonation pretreatment before anaerobic digestion | O3: 0.1-0.4 gL-1 Optimum wastewater: 0.2 g O3 L-1 | Total phenolics reduced from 613 to 155 mg L-1 SCOD/TCOD: +14.5% Volumetric biogas yield: +67.0% | [84] |
| Struvite precipitation + Fenton oxidation | H2O2: 2680 mgL-1 Fe2+/H2O2 molar ratio: 0.8 Duration: 56 min | Soluble COD removal after the nutrient-recovery step: 76.0% | [85] |
| Peroxi-coagulation + H2O2 + nanofiltration | Acidic peroxi-coagulation stage (pH 3) with external H2O2, followed by nanofiltration | COD reduction: 86.3% Color, turbidity, and suspended-particle removal: > 99.0% Flux recovery ratio: ~ 96.0% | [86] |
| ZnO-lemongrass photocatalysis | ZnO-L = 0.1 g L-1; pH 8 | COD: 97.0% Turbidity: 85.6% Color removal: 50.9% | [87] |
| ZnO-lemongrass photocatalytic membrane reactor | Plant-extracted ZnO-L nanoparticles | Color removal with enhanced permeate flux and mitigation of membrane fouling: ~ 99.5% | [88] |
| Heterogeneous electro-Fenton, Cu-doped magnetic graphene oxide | Optimized electro-Fenton-like treatment: 90 min | COD: 89.0% TOC removal: 48.1% Removal efficiency retained after five reuse cycles: ~ 78.0% Reported cost: USD 1.10 kg-1 COD removed | [89] |
| TiO2-embedded dual-layer mullite hollow-fiber membrane | TiO2 dosage: 1-4 wt.% UV-Vis irradiation; Best-performing membrane contained: 4 wt.% TiO2 | COD: 44.9% Color removal: 52.4% Flux: ~ 18.90 Lm-2h-1bar-1 | [90] |
Photocatalytic treatment has demonstrated considerable potential for POME remediation, particularly when the organic loading is reduced before irradiation. A ZnO/Zn-based photocatalytic fuel cell operated at pH 7, a contact time of 6 h and a light intensity of 1,300 lx achieved approximately 74.0% COD removal from diluted POME while simultaneously producing electrical energy[82]. However, the treatment efficiency decreased substantially when the initial POME concentration increased, indicating that excessive organic loading can inhibit photocatalytic reactions through light attenuation, occupation of active catalyst sites and deposition of organic matter on the photoanode surface. This observation supports the use of photocatalysis primarily as a polishing treatment rather than as a stand-alone process for untreated high-strength POME. The importance of wastewater matrix effects is also evident in visible-light photocatalytic systems. Modified semiconductor photocatalysts can improve visible-light absorption and enhance the generation of reactive oxygen species, but their performance in real treated POME generally remains lower than that obtained using model pollutant solutions. The complex composition of treated POME, including residual dissolved organic matter, suspended particles and competing radical scavengers, can suppress photocatalytic reactions even when highly active photocatalysts are employed. Recent reviews therefore identify limited visible- and solar-light utilization, catalyst recovery, fouling and scale-up as major challenges restricting the practical application of photocatalytic POME treatment[91].
Persulfate-based oxidation represents another effective approach for treating biologically treated POME because activated persulfate generates sulfate radicals with a high oxidation potential and comparatively long lifetime. Under optimized thermal activation conditions of approximately 67.4 °C, an S2O82-/COD ratio of 9.8 and a reaction time of 120 min, COD and color removals exceeding 85.0% have been reported[83]. Sulfate-radical oxidation can effectively degrade residual refractory organic matter after biological treatment. Nevertheless, the relatively high persulfate requirement and thermal energy demand may increase operating costs, thereby limiting its economic attractiveness for large-volume POME treatment unless waste heat or other low-cost thermal sources are available. Ozonation has shown a different but complementary role in POME treatment. Rather than solely aiming for maximum COD removal, controlled ozonation can selectively oxidize phenolic and other inhibitory compounds and increase the biodegradability of POME. An ozone dosage of approximately 0.2 g O3 L-1 of wastewater substantially modified the phenolic composition of POME, increased the soluble-to-total COD ratio by 14.5% and subsequently enhanced volumetric biogas production by 67.0% during anaerobic fermentation[84]. This result demonstrates an important treatment strategy in which AOPs are used for partial oxidation and detoxification rather than complete mineralization because this approach reduces the oxidant requirement while the remaining biodegradable organic matter is subsequently converted into methane through anaerobic digestion. The broader POME-AOP literature similarly identifies ozonation as a promising technology because pollutants can be degraded directly in the aqueous phase without requiring transfer onto a secondary adsorbent or concentrate stream[92].
Fenton oxidation has demonstrated substantial removal of refractory soluble organic matter from anaerobically treated POME. When applied following struvite precipitation, optimum conditions of approximately 2,680 mg L-1 H2O2, an Fe2+/H2O2 molar ratio of 0.8 and a reaction time of 56 min resulted in approximately 76.0% soluble COD removal[85]. The sequential configuration is particularly significant because it separates resource recovery from pollutant destruction. Ammoniacal nitrogen is first recovered through struvite precipitation, while the subsequent Fenton stage oxidizes the residual refractory carbon. This treatment arrangement is preferable to describing Fenton oxidation itself as a resource-recovery technology because its primary function is degradation of dissolved organic pollutants. However, conventional Fenton treatment still involves high chemical consumption and generation of iron-containing sludge, which can increase treatment and disposal costs. Recent developments in heterogeneous electro-Fenton treatment seek to overcome some of these limitations by improving catalyst recovery and reuse. A Cu-doped magnetic graphene oxide catalyst applied to anaerobically digested POME achieved approximately 89.0% COD removal within 90 min, while maintaining approximately 78.0% removal performance after five reuse cycles[89]. The magnetic characteristics of the catalyst facilitate separation from the treated wastewater and therefore provide an advantage over conventional homogeneous iron-based Fenton systems. The same study reported a treatment cost of approximately USD 1.10 kg-1 COD removed, suggesting that catalyst recovery and repeated reuse could contribute to improved process economics. Nevertheless, long-term catalyst stability, potential metal leaching and performance under continuous-flow operating conditions remain important issues requiring further investigation.
Photocatalytic membrane reactors represent another promising hybrid configuration. Recent ZnO-based photocatalytic membrane systems applied to anaerobically treated POME have achieved very high color removal, reaching approximately 99.5% under optimized operating conditions, while simultaneously improving permeate flux and reducing membrane fouling[88]. The integration of photocatalysis with membrane separation can therefore address two common limitations of suspended photocatalytic systems, namely catalyst recovery and post-treatment solid separation. Nevertheless, the long-term stability of immobilized photocatalysts, catalyst deactivation, membrane fouling and energy demand associated with irradiation remain important considerations before large-scale application can be justified. Hybrid treatment systems integrating AOPs with membrane separation have increasingly been explored because they simultaneously provide organic degradation and physical contaminant separation. A peroxi-coagulation-nanofiltration configuration applied to anaerobically treated POME achieved approximately 86.0% overall COD reduction together with more than 99.0% removal of color, turbidity and suspended particles[86]. In this type of treatment train, however, the high removal efficiencies should not be attributed entirely to advanced oxidation because coagulation, precipitation and membrane rejection also contribute significantly to pollutant removal. Consequently, performance data from hybrid systems should be interpreted as overall treatment efficiency rather than direct evidence of oxidative mineralization.
Recent studies indicate that AOP performance is strongly dependent on the degree of upstream POME treatment. High treatment efficiencies are generally obtained when AOPs are applied to diluted, anaerobically treated, biologically treated or final-discharge POME rather than to untreated raw POME. This is consistent with the characteristics of raw POME, which contains very high concentrations of organic matter, suspended solids and colored compounds capable of rapidly consuming oxidants, scavenging radicals and restricting light penetration. Photocatalysis, Fenton oxidation, sonocatalysis, sonophotocatalysis and ozonation have consequently been proposed primarily for advanced treatment and mineralization of residual pollutants rather than for bulk organic-load removal[92]. COD, color, and turbidity removal are commonly reported as the principal performance indicators, but these parameters do not demonstrate that the organic pollutants have been completely converted into CO2, water and inorganic species. COD reduction can also arise from partial oxidation, coagulation, precipitation or membrane retention, while colored compounds may be transformed into colorless intermediates that still contain substantial organic carbon. Measurements including total organic carbon removal, identification of transformation products, biodegradability indices and toxicity assessment are therefore necessary to confirm the extent of mineralization.
AOPs are positioned as tertiary polishing, detoxification or pretreatment processes within integrated POME treatment systems. Biological processes remain more practical for removing the bulk biodegradable organic load, whereas AOPs can target refractory compounds, residual color and phenolic substances that are resistant to conventional treatment. Integration of AOPs with anaerobic digestion can enhance subsequent methane recovery, while combinations with nutrient precipitation or membrane treatment can provide additional opportunities for resource recovery and water reuse. Future research should therefore move beyond achieving high laboratory-scale removal percentages and focus on continuous-flow operation, real final-discharge POME, catalyst lifetime, oxidant consumption, electrical-energy requirements, treatment costs, degradation-product toxicity and pilot-scale validation.
CHALLENGES OF CURRENT POME TREATMENT TECHNOLOGY
Conventional POME treatment can provide inadequate control of residual pollution[15]. New treatment methods increasingly combine pollutant removal with resource recovery[11]. Anaerobic digestion produces biogas but depends on balanced microbial activity and controlled temperature, pH, loading, and retention time. Changes in POME composition can disrupt the microbial community and reduce gas yield and process stability. More resilient microbial consortia and improved process control are therefore required. Membrane bioreactors, adsorption, and biological nutrient-recovery systems provide complementary treatment functions but face distinct operational and economic constraints.
Membrane bioreactors produce high-quality effluent by integrating biological degradation with membrane-based solid-liquid separation. However, membrane fouling reduces permeate flux and increases the frequency of backwashing, chemical cleaning, and membrane replacement. Fouling results from cake-layer formation, pore blockage, microbial attachment, extracellular polymeric substances, soluble microbial products, membrane properties, and operating conditions[93]. Fouling-resistant membrane materials, optimized cleaning protocols, and energy-efficient fouling-control strategies are therefore required to reduce operating costs and extend membrane service life[93].
Adsorption provides an operationally simple method for removing contaminants from POME, but its classification as resource recovery requires the subsequent release and utilization of the captured material. Spent-adsorbent management remains a major limitation because regeneration efficiency, contaminant desorption, adsorbent deterioration, secondary waste generation, and final disposal affect overall process sustainability. Future studies should quantify desorption efficiency, nutrient concentration in the recovered solution, adsorbent regeneration efficiency, and performance over repeated adsorption-desorption cycles[94]. Hybrid biological and advanced-oxidation systems can improve the treatment of complex wastewater containing biodegradable and recalcitrant contaminants, although their energy demand and process compatibility require evaluation[95].
Nutrient removal using microalgae and aquatic plants is constrained by light availability, inhibitory wastewater constituents, biomass harvesting, culture stability, environmental variability, and integration with existing treatment systems[96]. High biomass concentrations, suspended solids, and inadequate mixing restrict light penetration and reduce photosynthetic productivity, whereas closed photobioreactors require greater capital investment and operational control. Excess ammonia and other wastewater contaminants can inhibit microalgal growth, while variations in nutrient composition, temperature, irradiance, and pH affect biomass productivity and treatment performance. Microalgal harvesting remains a major scale-up constraint because centrifugation and membrane separation have high energy and operating requirements. Floating aquatic macrophytes require regular harvesting to maintain plant density, preserve treatment capacity, and remove accumulated nutrients from the treatment system[97]. Outdoor systems are also affected by temperature, irradiance, nutrient availability, culture composition, and biological contamination. Commercial application therefore requires low-energy biomass harvesting, stable outdoor cultivation, safe biomass processing, and defined markets for recovered biomass products[97].
EMERGING TECHNOLOGIES AND PROSPECTS
Future research should prioritize commercial-scale POME recovery pathways that generate and capture usable products, particularly biogas, biomass, and biologically produced chemicals. Adsorption studies should quantify desorption, regeneration, nutrient concentration, recovery yield, and reuse of nutrient-loaded adsorbents. Studies using microalgae and aquatic plants should quantify nutrient partitioning into harvested biomass, harvesting efficiency, biomass quality, and end-use performance. Advanced oxidation research should optimize pollutant degradation, energy demand, reagent consumption, toxicity reduction, and biodegradability. Techno-economic and life-cycle assessments are needed to compare the treatment and recovery functions of integrated POME biorefineries.
Combining anaerobic and aerobic treatment can improve POME treatment performance[98]. Anaerobic treatment reduces complex organic matter and produces biogas, after which aerobic treatment oxidizes residual biodegradable compounds. A pilot-scale integrated anaerobic-aerobic bioreactor started within 24 days and operated at organic loading rates up to 30.0 g-COD/(L·day)[98]. Process simulation and optimization have also examined biogas production and economic and environmental performance[99]. Further development should optimize solids retention time, recirculation, and temperature and validate performance at commercial scale. Adding biochar to bioreactors can support POME treatment [Figure 3]. In anaerobic systems, biochar provides a porous surface for microbial attachment and can adsorb inhibitory organic compounds and nutrients[100]. These functions can improve process stability and biogas production. In aerobic treatment, biochar can remove dissolved contaminants[101]. However, the overall environmental benefit depends on biochar production, dosage, regeneration or disposal, and the energy and chemical requirements of the treatment system[102].
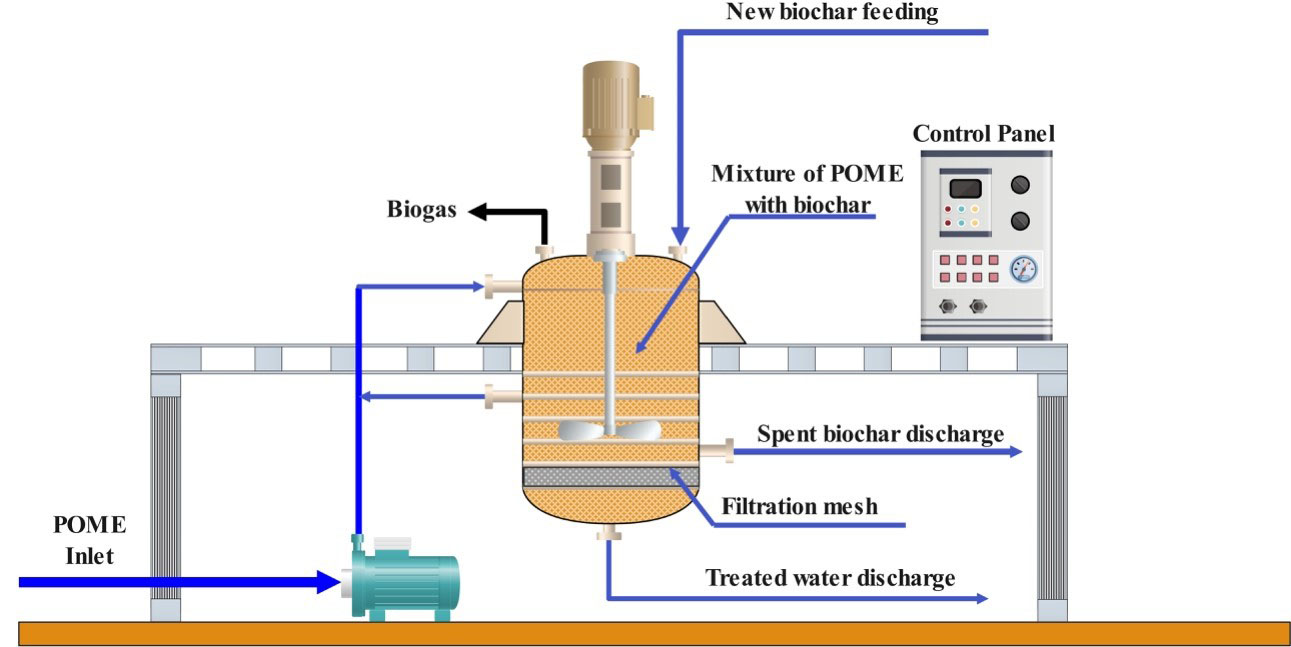
Figure 3. Biochar-amended bioreactor integrated with a filtration mesh. POME: Palm oil mill effluent.
AOPs can polish treated POME by degrading persistent organic compounds, reducing color, and improving biodegradability[70,103]. Ozonation, Fenton oxidation, and ultraviolet/H2O2 treatment generate reactive species that break down organic pollutants. Their implementation requires control of reagent dosage, pH, reaction time, and energy use. Future POME studies should report mineralization, residual toxicity, biodegradability, oxidant and catalyst consumption, energy demand, and secondary residues in addition to chemical oxygen demand and color removal. Adsorption research should progress from removal efficiency to demonstrated recovery by quantifying desorption conditions, nutrient concentration in the regenerant, recovery yield, adsorbent regeneration over repeated cycles, and spent-adsorbent management. Direct agricultural use of nutrient-loaded biochar or other adsorbents requires evidence of nutrient release, crop response, contaminant safety, and soil compatibility. Biological nutrient-recovery studies should report biomass productivity, harvesting efficiency, nitrogen and phosphorus content of the harvested biomass, and the fraction of influent nutrients recovered. Proposed uses as biofertilizer, feed, or biofuel also require product-composition, safety, performance, and downstream-processing data. Emerging biological nutrient-recovery technologies focus on reactor design, strain selection, integration with membrane separation, and lower-energy biomass harvesting. Photobioreactors can use controlled lighting and sensors to maintain growth conditions, while hybrid membrane systems retain biomass and improve nutrient removal. Floating treatment wetlands and constructed wetlands use plants and rhizosphere microorganisms to assimilate nutrients. These approaches require POME-specific validation of nutrient recovery, biomass quality, energy demand, operating stability, and commercial-scale performance.
Figure 4 presents an integrated POME treatment concept in which each unit operation performs a distinct function. Anaerobic digestion reduces the organic load and produces recoverable biogas. Aerobic treatment, advanced oxidation, coagulation and flocculation, and membrane filtration primarily reduce residual pollutants and polish the effluent. Adsorption transfers dissolved contaminants to a solid phase and contributes to resource recovery only when the loaded adsorbent is regenerated with product recovery or is beneficially reused. These pollutant-removal processes support the biorefinery by enabling water reuse and protecting operations that recover energy, biomass, nutrients, or chemicals.
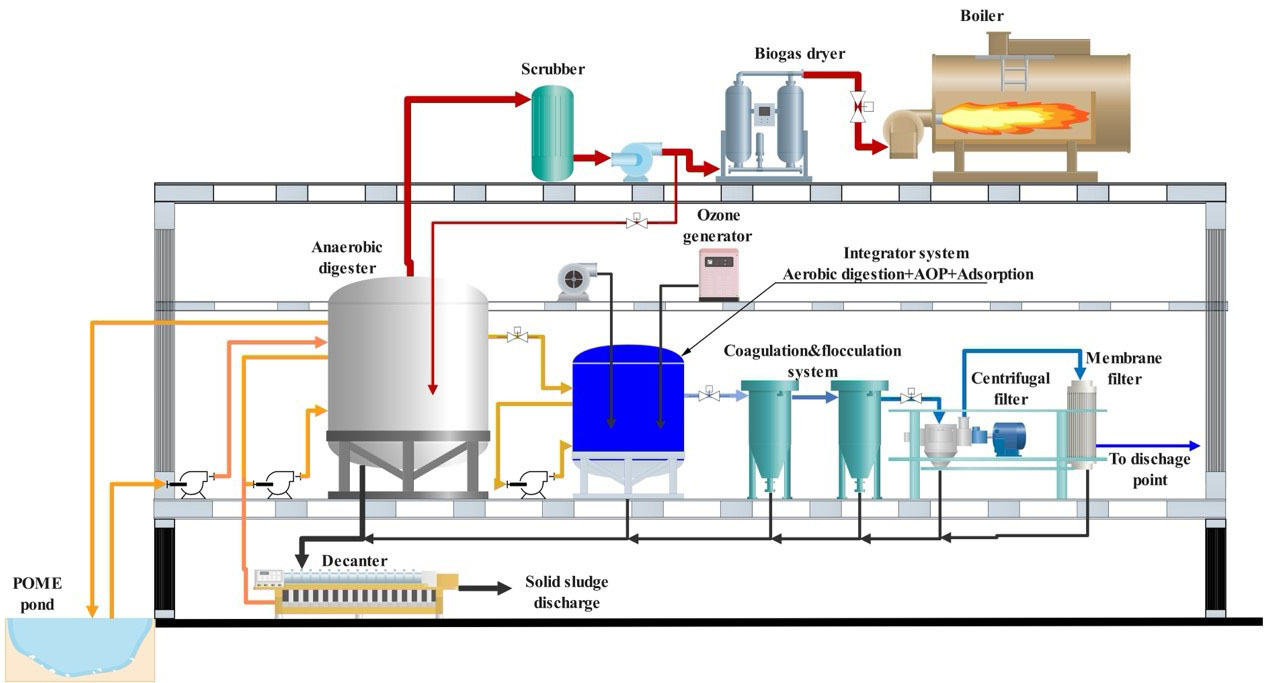
Figure 4. Proposed integrated treatment system for POME. POME: POME: Palm oil mill effluent; AOP: advanced oxidation process.
Hybrid treatment trains can increase nutrient capture from POME. Photobioreactor effluent can feed constructed wetlands, where plants and associated microorganisms remove remaining nutrients. Chemical crystallization can then recover phosphorus as struvite. However, the viability of these integrated systems depends on demonstrated mass balances, product quality, energy demand, capital and operating costs, and performance under field conditions. These data are required before modular treatment systems can be considered reliable resource-recovery platforms. Reorienting POME management from pollutant mitigation towards integrated treatment and resource recovery can provide environmental and resource benefits. Direct recovery is most clearly demonstrated for methane, hydrogen, and biologically produced organic acids. Advanced oxidation processes primarily provide pollutant degradation and polishing, whereas adsorption and microalgal or plant-based treatment capture nutrients that require subsequent recovery. Future POME biorefinery studies should report product yield, recovery efficiency, regeneration or harvesting performance, product quality, techno-economic performance, and life-cycle impacts alongside conventional treatment metrics.
CONCLUSION AND OUTLOOK
Integrated POME management can provide environmental and economic benefits when treatment systems recover usable energy, nutrients, biomass, or chemicals. Anaerobic digesters directly recover methane and hydrogen, while membrane bioreactors, adsorption, biological uptake, and advanced oxidation provide complementary separation and polishing functions. Claims of nutrient recovery require downstream evidence of desorption, regeneration, biomass harvesting, product quality, or beneficial reuse. Commercial implementation depends on technology maturity, scale, product markets, energy prices, and treatment costs. Future work should therefore combine process optimization with pilot- or industrial-scale validation, techno-economic analysis, and life-cycle assessment. Hybrid and multistage treatment systems should be designed around clearly defined treatment and recovery functions rather than removal efficiency alone.
DECLARATIONS
Acknowledgments
Su Shiung Lam acknowledges Chandigarh University for the grant support of adjunct professorship scheme (LAM/2/23) provided by the University Center for Research & Development.
Authors’ contributions
Conceptualization: Yek, P. N. Y.; Foong, S. Y.; Chan Y. H.; Chin, B. L. F.; Lock, S. S. M.; Kong, S. H.; Yiin, C. L.
Methodology: Yek, P. N. Y.; Foong, S. Y.; Chan Y. H.; Chin, B. L. F.; Lock, S. S. M.; Kong, S. H.; Yiin, C. L.
Investigation: Yek, P. N. Y.; Foong, S. Y.; Chan Y. H.; Chin, B. L. F.; Lock, S. S. M.; Kong, S. H.; Yiin, C. L.
Data acquisition: Yek, P. N. Y.; Foong, S. Y.; Chan Y. H.; Chin, B. L. F.; Lock, S. S. M.; Kong, S. H.; Yiin, C. L.
Writing - original draft: Yek, P. N. Y.; Foong, S. Y.; Chan Y. H.; Chin, B. L. F.; Lock, S. S. M.; Kong, S. H.; Yiin, C. L.
Funding acquisition: Wong, C. S.; Lam, S. S.
Review and editing: Wong, C. S.; Lam, S. S.
Availability of data and materials
Not applicable.
AI and AI-assisted tools statement
During the preparation of this manuscript, the AI tools Codex (GPT-5.6 Sol, released 2026-07-09) and Claude (Opus 5.5, released 2026-09-22) were used for language editing and to assist in developing the Graphical Abstract. The authors reviewed and edited the AI-assisted graphical content before incorporating it into the final Graphical Abstract. These tools were not used for study design, data collection, data analysis, or scientific interpretation. All authors take full responsibility for the accuracy, integrity, and final content of the manuscript.
Financial support and sponsorship
Universiti Malaysia Terengganu and Curtin University Malaysia are acknowledged for supporting this work through Matching Grant 1 + 3 (UMT/MG1+3/2023/53550). The authors also thank the University of Technology Sarawak for financial support through the UTS Internal Research Grant (UCTS/RESEARCH/1/2023/03).
Conflicts of interest
Lam, S. S. is an Associate Editor of Advanced Energy Conversion. Lam, S. S. was not involved in any steps of editorial processing, notably including reviewers’ selection, manuscript handling, and decision-making. Chan, Y, H. is affiliated with PETRONAS Research Sdn. Bhd. The other authors declare that there are no conflicts of interest.
Ethical approval and consent to participate
Not applicable.
Consent for publication
Not applicable.
Copyright
© The Author(s) 2026.
REFERENCES
1. Rajakal, J. P.; Hwang, J. Z. H.; Hassim, M. H.; Andiappan, V.; Tan, Q. T.; Ng, D. K. Integration and optimisation of palm oil sector with multiple-industries to achieve circular economy. Sustain. Prod. Consump. 2023, 40, 318-36.
2. Kadir, A. P. G. 2024. Overview of the Malaysian oil plam industry in 2024. https://bepi.mpob.gov.my (accessed 2026-10-27).
3. Khatun, R.; Reza, M. I. H.; Moniruzzaman, M.; Yaakob, Z. Sustainable oil palm industry: the possibilities. Renew. Sustain. Energy. Rev. 2017, 76, 608-19.
4. Mahmod, S. S.; Takriff, M. S.; Al-rajabi, M. M.; et al. Water reclamation from palm oil mill effluent (POME): recent technologies, by-product recovery, and challenges. J. Water. Process. Eng. 2023, 52, 103488.
5. Suksaroj, C.; Jearat, K.; Cherypiew, N.; Rattanapan, C.; Suksaroj, T. T. Promoting circular economy in the palm oil industry through biogas codigestion of palm oil mill effluent and empty fruit bunch pressed wastewater. Water 2023, 15, 2153.
6. A Aziz, M. M.; Kassim, K. A.; Elsergany, M.; et al. Recent advances on palm oil mill effluent (POME) pretreatment and anaerobic reactor for sustainable biogas production. Renew. Sustain. Energy. Rev. 2020, 119, 109603.
7. Lanan, F. A. B. M.; Selvarajoo, A.; Sethu, V.; Arumugasamy, S. K. Utilisation of natural plant-based fenugreek (Trigonella foenum-graecum) coagulant and okra (Abelmoschus escluentus) flocculant for palm oil mill effluent (POME) treatment. J. Environ. Chem. Eng. 2021, 9, 104667.
8. Sani, K.; Kongjan, P.; Pakhathirathien, C.; et al. Effectiveness of using two-stage anaerobic digestion to recover bio-energy from high strength palm oil mill effluents with simultaneous treatment. J. Water. Process. Eng. 2021, 39, 101661.
9. Farid, M. A. A.; Zakaria, M. R.; Hassan, M. A.; et al. A holistic treatment system for palm oil mill effluent by incorporating the anaerobic-aerobic-wetland sequential system and a convective sludge dryer. Chem. Eng. J. 2019, 369, 195-204.
10. Ng, K. H.; Yuan, L. S.; Cheng, C. K.; Chen, K.; Fang, C. TiO2 and ZnO photocatalytic treatment of palm oil mill effluent (POME) and feasibility of renewable energy generation: a short review. J. Clean. Prod. 2019, 233, 209-25.
11. Soo, P. L.; Bashir, M. J. K.; Wong, L. P. Recent advancements in the treatment of palm oil mill effluent (POME) using anaerobic biofilm reactors: challenges and future perspectives. J. Environ. Manage. 2022, 320, 115750.
12. Khongkhaem, P.; Suttinun, O.; Intasiri, A.; Pinyakong, O.; Luepromchai, E. Degradation of phenolic compounds in palm oil mill effluent by silica-immobilized bacteria in internal loop airlift bioreactors. CLEAN. Soil. Air. Water. 2016, 44, 383-92.
13. Nagime, P. V.; Upaichit, A.; Cheirsilp, B.; Boonsawang, P. Bio-succinic acid production from palm oil mill effluent using enterococcus Gallinarum with sequential purification of biogas. Fermentation 2023, 9, 369.
14. Mohd-Nor, D.; Ramli, N.; Sharuddin, S. S.; et al. Dynamics of microbial populations responsible for biodegradation during the full-scale treatment of palm oil mill effluent. Microbes. Environ. 2019, 34, 121-8.
15. Mohammad, S.; Baidurah, S.; Kobayashi, T.; Ismail, N.; Leh, C. P. Palm oil mill effluent treatment processes - a review. Processes 2021, 9, 739.
16. Sahil, S.; Singh, R.; Masakapalli, S. K.; et al. Biomass pretreatment, bioprocessing and reactor design for biohydrogen production: a review. Environ. Chem. Lett. 2024, 22, 1665-702.
17. Syahin, M. S.; Wan Ab Karim Ghani, W. A.; Loh, S. K. Decolourisation of palm oil mill effluent (pome) treatment technologies: a review. J. Oil. Palm. Res. 2020, 32, 1-15.
18. Lokman, N. A.; Ithnin, A. M.; Yahya, W. J.; Yuzir, M. A. A brief review on biochemical oxygen demand (BOD) treatment methods for palm oil mill effluents (POME). Environ. Technol. Innovation. 2021, 21, 101258.
19. Dashti, A. F.; Aziz, H. A.; Ibrahim, A. H.; Zahed, M. A. Suspended solid removal of palm oil mill effluent using horizontal roughing filter and calcinated limestone. Water. Air. Soil. Pollut. 2020, 231, 4755.
20. Onyla, C.; Uyub, A.; Akunna, J.; Norulaini, N.; Omar, A. Increasing the fertilizer value of palm oil mill sludge: bioaugmentation in nitrification. Water. Sci. Technol. 2001, 44, 157-62.
21. Jagaba, A.; Kutty, S.; Hayder, G.; et al. Sustainable use of natural and chemical coagulants for contaminants removal from palm oil mill effluent: a comparative analysis. Ain. Shams. Eng. J. 2020, 11, 951-60.
22. Akhbari, A.; Kutty, P. K.; Chuen, O. C.; Ibrahim, S. A study of palm oil mill processing and environmental assessment of palm oil mill effluent treatment. Environ. Eng. Res. 2020, 25, 212-21.
23. Hossen, M. A.; Yaacof, N.; Azahar, F. N.; Ahmad, N.; Aziz, A. A. Removal of ammoniacal nitrogen from Malaysian palm oil mill effluent (POME) using optimized operating parameters of peat soil as natural adsorbent. Cleaner. Water. 2024, 2, 100031.
24. Elvitriana; Yaacof, N.; Munir, E.; Delvian; Wahyuningsih, H. Organic substances reduction in palm oil mill effluent (POME) after cultivation with locally isolated microalgae. ARFMTS 2021, 80, 98-105.
25. Wongfaed, N.; Kongjan, P.; Suksong, W.; Prasertsan, P.; O-Thong, S. Strategies for recovery of imbalanced full-scale biogas reactor feeding with palm oil mill effluent. PeerJ 2021, 9, e10592.
26. Lee, Z. S.; Chin, S. Y.; Lim, J. W.; Witoon, T.; Cheng, C. K. Treatment technologies of palm oil mill effluent (POME) and olive mill wastewater (OMW): a brief review. Environ. Technol. Innovation. 2019, 15, 100377.
27. Khongkliang, P.; Chalearmkul, K.; Boonloh, K.; et al. Performance of combined organic precipitation, electrocoagulation, and electrooxidation in treating anaerobically treated palm oil mill effluents. Appl. Water. Sci. 2024, 14, 2288.
28. Zaied, B.; Siddique, M.; Zularisam, A.; Ahmad, M.; Salih, Y. Biomethane production from anaerobic codigestion of palm oil mill effluent with cattle manure: a review. Asian. J. Chem. 2019, 31, 2413-24.
29. Hariz, H. B.; Takriff, M. S.; Yasin, N. H. M.; Ba-Abbad, M. M.; Hakimi, N. I. N. M. Potential of the microalgae-based integrated wastewater treatment and CO2 fixation system to treat Palm Oil Mill Effluent (POME) by indigenous microalgae; Scenedesmus sp. and Chlorella sp. J. Water. Process. Eng. 2019, 32, 100907.
30. Hashiguchi, Y.; Zakaria, M. R.; Maeda, T.; Yusoff, M. Z. M.; Hassan, M. A.; Shirai, Y. Toxicity identification and evaluation of palm oil mill effluent and its effects on the planktonic crustacean Daphnia magna. Sci. Total. Environ. 2020, 710, 136277.
31. Hashiguchi, Y.; Zakaria, M. R.; Toshinari, M.; Yusoff, M. Z. M.; Shirai, Y.; Hassan, M. A. Ecotoxicological assessment of palm oil mill effluent final discharge by zebrafish (Danio rerio) embryonic assay. Environ. Pollut. 2021, 277, 116780.
32. Iskandar, M. J.; Baharum, A.; Anuar, F. H.; Othaman, R. Palm oil industry in south east Asia and the effluent treatment technology - a review. Environ. Technol. Innovation. 2018, 9, 169-85.
33. Yusof, M. A. B.; Chan, Y. J.; Chong, C. H.; Chew, C. L. Effects of operational processes and equipment in palm oil mills on characteristics of raw palm oil mill effluent (POME): a comparative study of four mills. Clean. Waste. Syst. 2023, 5, 100101.
34. Nahrul, Z. H.; Ibrahim, M.; Faizah, J. N.; et al. Palm oil mill final discharge treatment by a continuous adsorption system using oil palm kernel shell activated carbon produced from two-in-one carbonization activation reactor system. J. Water. Process. Eng. 2020, 36, 101262.
35. Isa, M. H.; Bashir, M. J. K.; Wong, L. P. Anaerobic treatment of ultrasound pretreated palm oil mill effluent (POME): microbial diversity and enhancement of biogas production. Environ. Sci. Pollut. Res. Int. 2022, 29, 44779-93.
36. Chin, M. J.; Poh, P. E.; Tey, B. T.; Chan, E. S.; Chin, K. L. Biogas from palm oil mill effluent (POME): opportunities and challenges from Malaysia’s perspective. Renew. Sustain. Energy. Rev. 2013, 26, 717-26.
37. Zainal, N. H. A review on the development of palm oil mill effluent (POME) final discharge polishing treatments. J. Oil. Palm. Res. 2018, 29, 528-40.
38. Jumadi, J.; Kamari, A.; Wong, S. T. S. Water quality assessment and a study of current palm oil mill effluent (POME) treatment by ponding system method. IOP. Conf. Ser:. Mater. Sci. Eng. 2020, 980, 012076.
39. Nasir, M. A.; Jahim, J. M.; Abdul, P. M.; Silvamany, H.; Maaroff, R. M.; Yunus, M. F. M. The use of acidified palm oil mill effluent for thermophilic biomethane production by changing the hydraulic retention time in anaerobic sequencing batch reactor. Int. J. Hydrogen. Energy. 2019, 44, 3373-81.
40. Isa, M. H.; Wong, L. P.; Bashir, M. J. K.; et al. Improved anaerobic digestion of palm oil mill effluent and biogas production by ultrasonication pretreatment. Sci. Total. Environ. 2020, 722, 137833.
41. Khadaroo, S. N.; Grassia, P.; Gouwanda, D.; He, J.; Poh, P. E. Enhancing the biogas production and the treated effluent quality via an alternative palm oil mill effluent (POME) treatment process: integration of thermal pretreatment and dewatering. Biomass. Bioenerg. 2021, 151, 106167.
42. Yap, B.; Heng, G.; Ng, C.; Bashir, M.; Lock, S. Enhancement of electrochemical-anaerobic digested palm oil mill effluent waste activated sludge in solids minimization and biogas production: bench-scale verification. Processes 2023, 11, 1609.
43. Wadchasit, P.; Suksong, W.; O-Thong, S.; Nuithitikul, K. Development of a novel reactor for simultaneous production of biogas from oil-palm empty fruit bunches (EFB) and palm oil mill effluents (POME). J. Environ. Chem. Eng. 2021, 9, 105209.
44. Zainal, B. S.; Gunasegaran, K.; Tan, G. Y. A.; et al. Effect of temperature and hydraulic retention time on hydrogen production from palm oil mill effluent (POME) in an integrated up-flow anaerobic sludge fixed-film (UASFF) bioreactor. Environ. Technol. Innovation. 2022, 28, 102903.
45. Liew, Z. K.; Chan, Y. J.; Ho, Z. T.; et al. Biogas production enhancement by co-digestion of empty fruit bunch (EFB) with palm oil mill effluent (POME): performance and kinetic evaluation. Renew. Energy. 2021, 179, 766-77.
46. Kongjan, P.; Sama, K.; Sani, K.; Jariyaboon, R.; Reungsang, A. Feasibility of bio-hythane production by co-digesting skim latex serum (SLS) with palm oil mill effluent (POME) through two-phase anaerobic process. Int. J. Hydrogen. Energy. 2018, 43, 9577-90.
47. Yong, G. T. X.; Chan, Y. J.; Lau, P. L.; et al. Optimization of the performances of palm oil mill effluent (POME)-based biogas plants using comparative analysis and response surface methodology. Processes 2023, 11, 1603.
48. Yusof, M. A. B.; Chan, Y. J.; Chong, C. H. Comparative analysis in the performances of four in‐ground lagoon anaerobic digesters treating palm oil mill effluent (POME). Asia-Pacific. J. Chem. Eng. 2023, 18, e2947.
49. Krishnan, S.; Singh, L.; Sakinah, M.; et al. An investigation of two‐stage thermophilic and mesophilic fermentation process for the production of hydrogen and methane from palm oil mill effluent. Env. Prog. and. Sustain. Energy. 2017, 36, 895-902.
50. Mamimin, C.; Singkhala, A.; Kongjan, P.; et al. Two-stage thermophilic fermentation and mesophilic methanogen process for biohythane production from palm oil mill effluent. Int. J. Hydrogen. Energy. 2015, 40, 6319-28.
51. Chit, V.; Tan, L. S.; Kiew, P. L.; Tsuji, T.; Funazukuri, T.; Lock, S. S. M. Advancing process intensification with high-frequency ultrasound: a mini-review of applications in biofuel production and beyond. Processes 2023, 11, 1236.
52. Zhu, Y.; Chen, R.; Li, Y. Y.; Sano, D. Virus removal by membrane bioreactors: a review of mechanism investigation and modeling efforts. Water. Res. 2021, 188, 116522.
53. Som, A. M.; Yahya, A. Kinetics and performance study of ultrasonic-assisted membrane anaerobic system using monod model for palm oil mill effluent (POME) treatment. Clean. Eng. Technol. 2021, 2, 100075.
54. Abdurahman, N. H.; Rosli, Y. M.; Azhari, N. H.; Hayder, G.; Norasyikin, I. A hybrid ultrasonic membrane anaerobic system (UMAS) development for palm oil mill effluent (POME) treatment. Processes 2023, 11, 2477.
55. Neoh, C. H.; Yung, P. Y.; Noor, Z. Z.; et al. Correlation between microbial community structure and performances of membrane bioreactor for treatment of palm oil mill effluent. Chem. Eng. J. 2017, 308, 656-63.
56. Chaipetch, W.; Khongnakorn, W.; Yirong, C.; Boonkan, J.; Jaiyu, A.; Heran, M. Performance of a high rate two-stage anaerobic membrane bioreactor (AnMBR) for the treatment of palm oil mill effluent. BioRes 2022, 17, 3398-412.
57. Yee, T. L.; Rathnayake, T.; Visvanathan, C. Performance evaluation of a thermophilic anaerobic membrane bioreactor for palm oil wastewater treatment. Membranes. (Basel). 2019, 9, 55.
58. Tai, C. Y.; Abuabdou, S. M.; Ng, C. A.; Gan, C. H.; Bashir, M. J. Performance of hybrid anaerobic membrane bioreactors (AnMBRs) augmented with activated carbon in treating palm oil mill effluent (POME). Desalin. Water. Treat. 2020, 202, 78-85.
59. Chaipetch, W.; Jaiyu, A.; Jutaporn, P.; Heran, M.; Khongnakorn, W. Fouling behavior in a high-rate anaerobic submerged membrane bioreactor (AnMBR) for palm oil mill effluent (POME) treatment. Membranes. (Basel). 2021, 11, 649.
60. Akpomie, K. G.; Conradie, J. Banana peel as a biosorbent for the decontamination of water pollutants. A review. Environ. Chem. Lett. 2020, 18, 1085-112.
61. Igwe, J.; Onyegbado, C.; Abia, A. Adsorption isotherm studies of BOD, TSS and colour reduction from palm oil mill effluent (POME) using boiler fly ash. Eclet. Quím. 2010, 35, 195-208.
62. Tan, Y. Y.; Bello, M. M.; Abdul Raman, A. A. Towards cleaner production in palm oil industry: advanced treatment of biologically-treated POME using palm kernel shell-based adsorbent. Clean. Eng. Technol. 2021, 2, 100079.
63. Razali, N.; Kamarulzaman, N. Z. Chemical characterizations of biochar from palm oil trunk for palm oil mill effluent (POME) treatment. Mater. Today:. Proc. 2020, 31, 191-7.
64. Zainal, N. H.; Aziz, A. A.; Idris, J.; et al. Reduction of POME final discharge residual using activated bioadsorbent from oil palm kernel shell. J. Clean. Prod. 2018, 182, 830-7.
65. Lam, S. S.; Liew, R. K.; Cheng, C. K.; et al. Pyrolysis production of fruit peel biochar for potential use in treatment of palm oil mill effluent. J. Environ. Manage. 2018, 213, 400-8.
66. Wahi, R.; Abdullah, L. C.; Mobarekeh, M. N.; Ngaini, Z.; Yaw, T. C. S. Utilization of esterified sago bark fibre waste for removal of oil from palm oil mill effluent. J. Environ. Chem. Eng. 2017, 5, 170-7.
67. Amosa, M. K. Process optimization of Mn and H2S removals from POME using an enhanced empty fruit bunch (EFB)-based adsorbent produced by pyrolysis. Environ. Nanotechnol. Monit. Manag. 2015, 4, 93-105.
68. Foo, N. S.; Loh, S. K.; Ismail, K.; Bachmann, R. T. Nutrient recovery from anaerobic palm oil mill effluent with thermally regenerated spent bleaching earth using response surface methodology. J. Oil. Palm. Res. 2020, 32, 245-57.
69. Budiman, P. M.; Wu, T. Y.; Ramanan, R. N.; Jahim, J. Md. Improvement of biohydrogen production through combined reuses of palm oil mill effluent together with pulp and paper mill effluent in photofermentation. Energy. Fuels. 2015, 29, 5816-24.
70. Bello, M. M.; Raman, A. A. A. Trend and current practices of palm oil mill effluent polishing: application of advanced oxidation processes and their future perspectives. J. Environ. Manage. 2017, 198, 170-82.
71. Luo, D.; Wang, L.; Nan, H.; et al. Phosphorus adsorption by functionalized biochar: a review. Environ. Chem. Lett. 2023, 21, 497-524.
72. Liu, Z.; Liu, H.; Zhang, Y.; Lichtfouse, E. Efficient phosphate recycling by adsorption on alkaline sludge biochar. Environ. Chem. Lett. 2023, 21, 21-30.
73. Said, M.; Abu Hasan, H.; Mohd Nor, M. T.; Mohammad, A. W. Removal of COD, TSS and colour from palm oil mill effluent (POME) using montmorillonite. Desalin. Water. Treat. 2016, 57, 10490-7.
74. Saifuddin, N.; Dinara, S. Pretreatment of palm oil mill effluent (POME) using magnetic chitosan. Journal. of. Chemistry. 2011, 8, S67-78.
75. Adeleke, A. O.; Latiff, A. A. A.; Al-Gheethi, A. A.; Daud, Z. Optimization of operating parameters of novel composite adsorbent for organic pollutants removal from POME using response surface methodology. Chemosphere 2017, 174, 232-42.
76. Mohd, N.; Yasin, N. H. M.; Osman, W. H. W.; Takriff, M. S. Unlocking the potential of Chlamydomonas sp. for sustainable nutrient removal from POME: a biokinetic investigation. J. Water. Process. Eng. 2024, 57, 104590.
77. Udaiyappan, A. F.; Hasan, H. A.; Takriff, M. S.; Sheikh Abdullah, S. R.; Mohd Yasin, N. H.; Ji, B. Cultivation and application of Scenedesmus sp. strain UKM9 in palm oil mill effluent treatment for enhanced nutrient removal. J. Clean. Prod. 2021, 294, 126295.
78. Kamyab, H.; Din, M. F. M.; Keyvanfar, A.; et al. Efficiency of microalgae chlamydomonas on the removal of pollutants from palm oil mill effluent (POME). Energy. Procedia. 2015, 75, 2400-8.
79. Al-Baldawi, I. A.; Yasin, S. R.; Jasim, S. S.; Abdullah, S. R. S.; Almansoory, A. F.; Ismail, N'. Removal kinetics of organic carbon from palm oil mill effluent by native duckweeds and its potential as a biofertilizer. J. Water. Process. Eng. 2023, 53, 103852.
80. Kadir, A. A.; Abdullah, S. R. S.; Othman, B. A.; et al. Dual function of Lemna minor and azolla pinnata as phytoremediator for palm oil mill effluent and as feedstock. Chemosphere 2020, 259, 127468.
81. Emparan, Q.; Harun, R.; Kodiappan, J. A. Effect of microalgae-to-palm oil mill effluent (POME) ratio for rapid effective pollutants removal and biomass production. Desalin. Water. Treat. 2020, 198, 119-25.
82. Moksin, N. S. A.; Ong, Y. P.; Ho, L.; Tay, M. G. Optimization of photocatalytic fuel cells (PFCs) in the treatment of diluted palm oil mill effluent (POME). J. Water. Process. Eng. 2021, 40, 101880.
83. Bashir, M. J. K.; Sheen, O. S.; Ng, C. A.; Abujazar, M. S. S.; Alazaiza, M. Y. D.; Abu Amr, S. S. Advanced treatment of palm oil mill effluent using thermally activated persulfate oxidation. Separations 2022, 9, 171.
84. Krishnan, S.; Homroskla, P.; Saritpongteeraka, K.; et al. Specific degradation of phenolic compounds from palm oil mill effluent using ozonation and its impact on methane fermentation. Chem. Eng. J. 2023, 451, 138487.
85. Sea, Y. F.; Chua, A. S. M.; Ngoh, G. C.; Rabuni, M. F. Integrated struvite precipitation and fenton oxidation for nutrient recovery and refractory organic removal in palm oil mill effluent. Water 2024, 16, 1788.
86. Ismail, S. A.; Chua, S. F.; Ang, W. L.; Mahmoudi, E.; Mohammad, A. W.; Wong, W. Y. Sequential peroxi-coagulation-nanofiltration treatment of anaerobically treated palm oil mill effluent (POME). J. Water. Process. Eng. 2024, 66, 105935.
87. Sidik, D. A. B.; Hairom, N. H. H.; Muhammad, A.; et al. Photocatalytic degradation of anaerobic treated palm oil mill effluent by modified ZnO with lemongrass and kinetic studies. J. Oil. Palm. Res. 2025, 38, 362-75.
88. Khiflie, N. N. S.; Sidik, D. A. B.; Hairom, N. H. H.; et al. Optimization of photocatalytic membrane-assisted plant extracted ZnO nanoparticles in treating anaerobically treated palm oil mill effluent. J. Phys. Chem. Solids. 2026, 216, 113780.
89. Wang, K. K.; Chai, P. V.; Ng, L. Y.; Thung, W. E.; Panpranot, J. Electro-Fenton treatment of anaerobic digested palm oil mill effluent using Cu-doped magnetic graphene oxide: Performance and techno-economic evaluation. J. Environ. Chem. Eng. 2026, 14, 122790.
90. Raji, Y. O.; Othman, M. H. D.; Puteh, M. H.; et al. Photocatalytic treatment of final discharge palm oil mill effluent (POME) using dual-layer hollow fiber ceramic membranes with TiO2-embedded mullite: Performance evaluation and mechanistic insights. Mater. Sci. Eng. B. 2026, 323, 118695.
91. Nawaz, R.; Kait, C. F.; Chia, H. Y.; et al. Countering major challenges confronting photocatalytic technology for the remediation of treated palm oil mill effluent: a review. Environ. Technol. Innovation. 2021, 23, 101764.
92. Vijayan, V.; Joseph, C. G.; Taufiq-Yap, Y. H.; et al. Mineralization of palm oil mill effluent by advanced oxidation processes: a review on current trends and the way forward. Environ. Pollut. 2024, 342, 123099.
93. Zielińska, M.; Ojo, A. Anaerobic membrane bioreactors (AnMBRs) for wastewater treatment: recovery of nutrients and energy, and management of fouling. Energies 2023, 16, 2829.
94. Ahmed, A. M.; Mekonnen, M. L.; Mekonnen, K. N. Polymer-based nanocomposite adsorbents for resource recovery from wastewater. RSC. Adv. 2023, 13, 31687-703.
95. Ponnusami, A. B.; Sinha, S.; Ashokan, H.; et al. Advanced oxidation process (AOP) combined biological process for wastewater treatment: a review on advancements, feasibility and practicability of combined techniques. Environ. Res. 2023, 237, 116944.
96. Sathinathan, P.; Parab, H.; Yusoff, R.; Ibrahim, S.; Vello, V.; Ngoh, G. Photobioreactor design and parameters essential for algal cultivation using industrial wastewater: a review. Renew. Sustain. Energy. Rev. 2023, 173, 113096.
97. Sayanthan, S.; Hasan, H. A.; Abdullah, S. R. S. Floating aquatic macrophytes in wastewater treatment: toward a circular economy. Water 2024, 16, 870.
98. Yap, C. C.; Chan, Y. J.; Loh, S. K.; et al. Pilot-scale investigation of the integrated anaerobic-aerobic bioreactor (IAAB) treating palm oil mill effluent (POME): startup and performance evaluation. Ind. Eng. Chem. Res. 2021, 60, 3839-59.
99. Chong, J. W. R.; Chan, Y. J.; Chong, S.; et al. Simulation and optimisation of integrated anaerobic-aerobic bioreactor (IAAB) for the treatment of palm oil mill effluent. Processes 2021, 9, 1124.
100. Chen, L.; Fang, W.; Liang, J.; et al. Biochar application in anaerobic digestion: Performances, mechanisms, environmental assessment and circular economy. Resour. Conserv. Recy. 2023, 188, 106720.
101. Lawal, A. A.; Hassan, M. A.; Farid, M. A. A.; et al. One-step steam pyrolysis for the production of mesoporous biochar from oil palm frond to effectively remove phenol in facultatively treated palm oil mill effluent. Environ. Technol. Innovation. 2020, 18, 100730.
102. Amalina, F.; Razak, A. S. A.; Krishnan, S.; Sulaiman, H.; Zularisam, A.; Nasrullah, M. Biochar production techniques utilizing biomass waste-derived materials and environmental applications - a review. J. Hazard. Mater. Adv. 2022, 7, 100134.
Cite This Article
 Open Access
How to Cite
Yek, P. N. Y.; Foong, S. Y.; Chan, Y. H.; Chin, B. L. F.; Lock, S. S. M.; Kong, S. H.; Yiin, C. L.; Wong, C. S.; Lam, S. S. Integrated treatment and resource recovery from palm oil mill effluent: technologies, performance, and future prospects. Adv. Energy Convers. 2026, 1, 10. https://dx.doi.org/10.20517/aec.2026.25
Download Citation
If you have the appropriate software installed, you can download article citation data to the citation manager of your choice. Simply select your manager software from the list below and click on download.
Export Citation File
Type of Import
Tips on Downloading Citation
Citation Manager File Format
Type of Import
Direct Import: When the Direct Import option is selected (the default state), a dialogue box will give you the option to Save or Open the downloaded citation data. Choosing Open will either launch your citation manager or give you a choice of applications with which to use the metadata. The Save option saves the file locally for later use.
Indirect Import: When the Indirect Import option is selected, the metadata is displayed and may be copied and pasted as needed.
About This Article
Copyright

Data & Comments
Data
0




Comments
Comments must be written in English. Spam, offensive content, impersonation, and private information will not be permitted. If any comment is reported and identified as inappropriate content by OAE staff, the comment will be removed without notice. If you have any queries or need any help, please contact us at [email protected].